What Are You Looking For?
内页banner
Blog
  • The Complete Guide to Leak-Resistant Paper Bowls with Lids for Food Delivery The Complete Guide to Leak-Resistant Paper Bowls with Lids for Food Delivery Oct 13, 2026
    Food delivery puts paper bowls through more demanding conditions than dine-in service. A bowl may hold hot soup, oily noodles, a freshly prepared grain bowl, or a chilled salad. It may then be sealed, stacked with other orders, carried in a delivery bag, and transported across town before the customer opens it. That journey is where packaging quality matters. A paper bowl can look sturdy on a shelf but still leak around its base, soften after prolonged contact with liquid, or lose its seal when the lid does not fit properly. For restaurants, food delivery brands, and packaging distributors, choosing the right bowl means looking at the entire packaging system—not just the paper material. This guide explains what makes leak-resistant paper bowls with lids suitable for food delivery, how coatings and lid design affect performance, and what buyers should test before placing a wholesale or custom order.   What Makes a Paper Bowl Leak-Resistant? A leak-resistant paper bowl combines several design features. The paperboard provides the structure, the inner coating helps resist moisture and grease, and the rim and base construction help prevent liquid from escaping through joints or weak points. The lid adds another layer of protection by covering the opening and helping reduce spills during handling. These features work together. A bowl with a suitable barrier coating can still leak if the base seam is poorly formed. Likewise, a well-made bowl may spill during delivery if the lid is the wrong size or has not been secured correctly. For food businesses, leak resistance should therefore be assessed under realistic use conditions. Consider the food's temperature, liquid content, oil level, holding time, and expected transportation distance before choosing a specification. Food delivery packaging needs to protect the contents from preparation through transportation. 1. Choose the Right Paper Bowl Coating The coating is one of the first details to review when sourcing paper bowls for delivery. Paper fibers naturally absorb moisture, so the bowl generally needs a suitable barrier when it is used for wet, oily, or hot foods. PE-coated paper bowls Polyethylene (PE) coatings are commonly used to improve moisture resistance. They can be suitable for many takeaway applications, depending on the bowl's construction and the intended food. Buyers should check whether the selected model is suitable for hot liquids, oily foods, and the required holding time. PLA-coated paper bowls Polylactic acid (PLA) is used in some paper food containers as an alternative coating material. It may be relevant to buyers exploring compostable packaging, but the environmental claims depend on the complete product, applicable certification, and available waste-treatment conditions. Do not assume every PLA-coated bowl is suitable for home composting or accepted by local composting facilities. Water-based barrier coatings Water-based coatings are another option for selected paper food packaging. Their performance varies by formulation and product design, so buyers should request technical information and conduct application-specific tests. Recyclability and compostability also depend on the coating, fiber recovery process, and local waste infrastructure. ElementsCup offers different paper bowl material and coating options, including PE, PP, PET, PLA, and water-based coatings. You can compare available options in the paper food bowls range and confirm the suitability of each specification with the supplier.   2. Match the Lid to the Bowl A lid is not simply an accessory. It is an essential part of a leak-resistant takeaway package. Even a durable bowl may spill if the lid is too loose, too tight to close properly, or incompatible with the rim design. When selecting paper bowls with lids, check the following: Rim compatibility: The lid should match the bowl's diameter and rim profile. Closure security: The lid should attach consistently without leaving gaps or becoming difficult for staff to close. Heat tolerance: Confirm that the lid material is suitable for the temperature of the food and the intended serving conditions. Stacking performance: Lidded bowls should remain stable when stacked or packed into delivery bags. Food visibility: Clear lids can help customers identify salads and prepared meals, while paper lids may suit other packaging needs. Not every lid is designed to be completely leakproof when inverted or shaken. If a restaurant delivers soups or sauces, it should test the assembled bowl and lid together rather than relying on a general product description.   A compatible lid helps reduce spills and keeps food covered during delivery. 3. Select the Bowl Shape and Capacity for the Menu The shape and size of a paper bowl influence both presentation and handling. A bowl that is too small may cause food to press against the lid. One that is too large can waste packaging space and allow the contents to move more during transportation. For soup, curry, and saucy noodles, buyers should prioritize a suitable depth, liquid capacity, and lid fit. For salads and grain bowls, a wider opening can make the contents easier to arrange and more appealing to customers. Rectangular bowls may work well for certain pasta dishes, meal portions, or food combinations that need a different presentation. Capacity alone does not tell the whole story. Two bowls with the same nominal volume may have different diameters, heights, and usable fill levels. Buyers should compare the actual dimensions and test with a typical serving before choosing a final size. For restaurants and distributors sourcing salad packaging, the paper salad bowls range includes different capacities for a variety of takeaway meals. Confirm the current dimensions and matching lid options for the selected model.     4. Test Leak Resistance Before Bulk Ordering Product samples are especially useful when selecting packaging for food delivery. A simple test plan can help identify problems before a large order reaches the kitchen or distribution warehouse. Fill test: Fill the bowl with the intended food or a suitable test liquid to the normal serving level. Holding test: Leave the contents in the bowl for the expected time before delivery, including a reasonable safety margin where appropriate. Base and seam inspection: Check the underside, sidewall joints, and base for moisture, softening, or leakage. Lid-fit test: Close the lid and inspect the rim for gaps. Check whether the lid remains secure during normal handling. Transport simulation: Place the assembled package in the type of delivery bag used by the business and simulate ordinary carrying and movement. Temperature check: Repeat testing with food at the expected serving temperature, following the product's stated use limits. These practical checks do not replace formal testing or food-contact compliance documentation. They help buyers evaluate whether a specific bowl and lid combination suits the intended application. For hot food, also confirm the product's temperature limits and any restrictions on reheating.   5. Consider Food Safety and Heating Requirements Leak resistance is only one part of food packaging performance. Materials that contact food must be suitable for the intended use and comply with the relevant requirements in the destination market. Before approving a product, request the available food-contact documentation and confirm which material and product configuration it covers. A document for one coating or bowl model should not automatically be treated as proof that every product in a supplier's range meets the same requirements. Microwave and oven suitability also require careful attention. Paper bowls are not automatically safe for every heating method. Suitability depends on the bowl's paperboard, coating, adhesives, printing, lid material, and the manufacturer's instructions. A bowl described as microwaveable may still need to be used without its lid, or within specific time and temperature limits. For delivery businesses that offer reheatable meals, verify the exact heating instructions and communicate them clearly to customers. Avoid assuming that a paper bowl suitable for hot food is also suitable for oven use.   6. Customization Options for Restaurants and Wholesale Buyers For food brands, packaging is part of the customer experience. Custom printing can help a bowl carry a logo, brand colors, promotional message, or product information. For distributors, offering several sizes and designs can make it easier to serve restaurants with different menus. When requesting a custom quotation, prepare the following details: Required capacity, bowl dimensions, and preferred shape. Food type, serving temperature, oil content, and expected holding time. Preferred paper material and barrier coating. Lid material, closure style, and required lid quantity. Printing artwork, colors, and packaging requirements. Estimated order volume, delivery destination, and target lead time. These details help the manufacturer recommend a suitable configuration and quote more accurately. Before mass production, confirm the final artwork, product specification, sample approval, and quality requirements in writing. For buyers who need a coordinated packaging solution, ElementsCup also provides other custom food packaging products. Ask the supplier about current customization capabilities, minimum order quantities, and compatible lid options.   Frequently Asked Questions Are paper bowls with lids leakproof? Some are designed to resist leakage, but performance depends on the bowl's coating, seams, rim construction, lid fit, and the food being packed. Test the complete bowl-and-lid combination under realistic delivery conditions before using it at scale. Which coating is best for paper bowls used for soup? The best coating depends on soup temperature, holding time, and the product's construction. PE, PP, PLA, PET, and water-based coatings have different properties and limitations. Request technical details and confirm suitability with the supplier. Can paper bowls with lids be used in the microwave? Only when the specific bowl is identified as suitable for microwave use. Check the manufacturer's instructions, temperature limits, and whether the lid must be removed. Do not assume every paper bowl or lid can be reheated safely. How can restaurants prevent paper bowls from leaking during delivery? Choose a bowl designed for the food, use a compatible lid, avoid overfilling, and follow the manufacturer's temperature and handling guidance. Conduct holding and transport tests with typical menu items before adopting a new package. Can paper bowls be customized for wholesale orders? Many suppliers offer different sizes, materials, coatings, and printing options. Buyers should confirm the available configurations, minimum order quantity, artwork requirements, lead time, and documentation for the exact product being ordered.   Choose Paper Bowls That Perform from Kitchen to Customer Reliable food delivery packaging starts with matching the bowl to the menu and the conditions it will face. The right combination of paperboard, barrier coating, bowl shape, and lid can help reduce leaks, protect food presentation, and make delivery handling more predictable. For restaurants, food service distributors, and private-label brands, sample testing is a practical way to compare options before placing a bulk order. Review the product specification, verify food-contact and heating requirements, and test the assembled package with the actual food whenever possible. ElementsCup offers paper food bowls and customization options for different food service applications. Contact the team with your target capacity, food type, lid preference, and estimated quantity to discuss a suitable packaging solution.  
  • What Is the Difference Between a Paper Cup Manufacturer and a Paper Cup Trading Company? What Is the Difference Between a Paper Cup Manufacturer and a Paper Cup Trading Company? Sep 24, 2026
    When sourcing disposable paper cups for a coffee shop, restaurant, catering business, foodservice distributor, or retail brand, you may come across two types of suppliers: a paper cup manufacturer and a paper cup trading company. Both can supply paper cups, but they do not operate in exactly the same way. A paper cup manufacturer is directly involved in production, while a trading company generally purchases products from manufacturing factories and supplies them to customers. For buyers placing custom or bulk orders, understanding this difference can make it easier to compare suppliers, communicate product requirements, evaluate quality control, and plan long-term purchasing. Elements Packaging is a paper cup and foodservice packaging manufacturer based in Xiamen, China. The company states that it has specialized in paper cup manufacturing and paper converting since 2008, with a 10,000-square-meter production facility. Its product range includes paper cups and other disposable foodservice packaging products. What Is a Paper Cup Manufacturer? A paper cup manufacturer is a company that directly operates or controls the manufacturing process used to produce paper cups. The production process may involve paper material selection, printing, coating or lining, cup forming, bottom sealing, quality inspection, packaging, and preparation for shipment. Because the manufacturer is connected directly to production, buyers can normally discuss technical specifications with the company that actually makes the product. This can be particularly important when an order involves custom sizes, printed artwork, special coatings, different cup structures, or specific packaging requirements. Elements' product range includes several paper cup structures and applications, including custom paper cups for hot and cold beverages. What Is a Paper Cup Trading Company? A paper cup trading company generally works as an intermediary between buyers and manufacturers. Instead of producing the paper cups itself, the trading company sources products from one or more factories and sells them to customers. A trading company can still provide valuable services. It may help with supplier selection, product sourcing, export documentation, logistics, communication, and order consolidation. For example, a buyer may need paper cups, food boxes, paper bags, and other packaging products from different factories. A trading company may coordinate these products through one commercial relationship. The main difference is therefore not simply the word used in the company's name. The more important question is who actually manufactures the product and who controls the production process? What Is the Difference Between a Paper Cup Manufacturer and a Trading Company? The most practical difference can be seen in production control, customization, quality management, and communication. Factor Paper Cup Manufacturer Trading Company Production Directly manufactures or controls production Purchases products from manufacturing suppliers Customization Specifications can be discussed directly with production Customization is coordinated through the factory Quality Control Direct involvement in production and inspection Usually depends on the manufacturing partner MOQ Based on production and customization requirements Depends on the selected factory and purchasing arrangement Lead Time Coordinated directly with production scheduling Depends on the manufacturing supplier Product Development Direct access to manufacturing capabilities Normally coordinated with the factory Does Buying Directly From a Paper Cup Manufacturer Always Cost Less? Not necessarily. The final price of a paper cup depends on much more than whether the supplier is a manufacturer or a trading company. Important cost factors can include: Paper material Cup size and structure Coating or lining Printing requirements Order quantity Packaging Customization Tooling requirements, when applicable Shipping terms A trading company may sometimes provide competitive pricing because it works with multiple factories or consolidates different products. A direct manufacturer may offer advantages when the buyer needs repeated production, detailed customization, or closer communication with the production side. For this reason, buyers should compare the complete sourcing cost and product specification, rather than choosing a supplier based only on the quoted unit price. Which Supplier Is More Suitable for Custom Paper Cups? When ordering custom paper cups, the supplier needs to understand more than just the desired quantity. A custom paper cup project may involve: Cup size and capacity Paper material Single wall or double wall construction Ripple wall or embossed structure Coating or lining Logo and artwork Printing colors Packaging method Application requirements Working with a manufacturer can make communication about these specifications more direct because the supplier is connected to the production process. For example, Elements offers custom double wall paper cups with options for size, color, logo, lining, and packaging. The product page currently lists sizes from 7oz to 20oz and different lining options. Why Does Quality Control Matter When Choosing a Paper Cup Supplier? Paper cups may look simple, but their performance depends on several manufacturing details. Material quality, coating, printing, cup forming, bottom sealing, rim construction, and packaging can all affect the finished product. For bulk buyers, quality consistency is especially important. A sample may look acceptable, but the real question is whether the same specifications can be maintained throughout mass production. When evaluating a paper cup manufacturer, buyers can ask about: Raw material specifications Production inspection procedures Finished product inspection Leakage or performance testing Available certifications Sample approval procedures Packaging and shipment inspection Elements states that its production and quality processes are used to support international foodservice customers, and its product range includes different material and coating options. Buyers should request the specific certificates and test documentation applicable to their market and intended use. What Should You Ask a Paper Cup Manufacturer Before Placing a Bulk Order? Before placing a large paper cup order, it is better to ask specific questions instead of simply requesting a price. A practical supplier checklist includes: What paper materials are available? What cup sizes can you produce? What coating or lining options are available? Can you customize the cup size and structure? Can you print my logo or artwork? What is the MOQ for custom paper cups? Can you provide samples before mass production? What is the normal production lead time? How is quality inspected during production? What certifications or test reports can you provide? How are finished cups packaged for export? Can you provide compatible lids and other packaging products? These questions help buyers understand the supplier's actual production capabilities instead of relying only on product photos or a quotation. Can a Paper Cup Manufacturer Provide Matching Lids? For beverage packaging, the cup and lid should be considered as one packaging system rather than two completely separate products. The lid needs to match the cup opening, fit securely, and support the intended beverage application. For takeaway coffee and other drinks, a poor fit can increase the risk of spills during transportation. Elements also produces paper cup lids in different sizes and designs. The company states that its paper lids are available in 62mm, 70mm, 80mm, and 90mm calibers, with customization available for specific requirements. Does the Type of Coating Matter When Choosing a Manufacturer? Yes. Coating or lining is an important part of paper cup specifications because it affects liquid resistance and the intended application of the cup. Depending on the product and market requirements, paper cups may use different lining or barrier technologies. Elements offers options including PE, PLA, and aqueous barrier coatings across its paper cup range. For buyers specifically looking for an alternative barrier technology, its aqueous barrier coating paper cups are designed for hot and cold beverage applications and can be customized in size, color, logo, lining, and packaging. Can a Paper Cup Manufacturer Supply Other Foodservice Packaging? Many manufacturers specialize in more than one type of disposable foodservice packaging. This can be useful for coffee shops, restaurants, catering companies, foodservice distributors, and brands that want to manage several packaging products through one supplier. Elements' product range extends beyond paper cups to include paper lids, paper bowls, paper food boxes, paper trays, paper bags, paper straws, and compostable cutlery. For foodservice businesses that also need takeaway packaging, the company's paper food boxes provide another product category that can be sourced alongside beverage packaging. When Does a Paper Cup Trading Company Make Sense? A trading company can be useful when a buyer needs a broad sourcing service rather than direct factory communication. For example, a buyer may need several types of packaging from different factories. A trading company may coordinate suppliers, consolidate products, arrange shipping, and handle export-related communication through one commercial contact. This model can be convenient for some purchasing projects. However, buyers should understand where the actual production takes place, especially when the order involves customized products, strict quality requirements, repeated production, or technical specifications. The important point is to evaluate the supplier based on its actual capabilities rather than simply relying on the label of “manufacturer” or “trading company.” How Can You Verify Whether a Paper Cup Supplier Is a Manufacturer? Before placing a large order, buyers can ask for practical information that helps verify manufacturing capability. Factory location and production facility information Production equipment or manufacturing process information Available product specifications Customization capabilities Quality control procedures Relevant certificates and test reports Sample development process Production capacity Typical lead time Factory audit or inspection options It is also useful to compare the supplier's stated manufacturing capabilities with the products shown on its website. A genuine paper cup manufacturer should be able to explain how different cup structures, materials, coatings, printing requirements, and packaging specifications are handled during production. Paper Cup Manufacturer or Trading Company: What Should Buyers Compare? The right sourcing model depends on the buyer's project requirements. A trading company may be useful for multi-product sourcing, supplier coordination, and logistics support. A direct manufacturer may be more relevant when a buyer needs customized products, detailed specifications, consistent production, or closer communication with the manufacturing side. When comparing paper cup suppliers, buyers should look beyond the initial quotation. Product material, cup structure, coating, customization, quality control, MOQ, lead time, certifications, packaging, and long-term supply capability all deserve attention. Elements Packaging states that it has specialized in paper cup manufacturing and paper converting since 2008 and operates a 10,000-square-meter production facility in Xiamen, China. Its current product range covers paper cups and multiple categories of disposable foodservice packaging. Frequently Asked Questions About Paper Cup Manufacturers and Trading Companies What is the main difference between a paper cup manufacturer and a trading company? A paper cup manufacturer directly produces or controls the production of paper cups, while a trading company generally sources finished products from manufacturing suppliers and sells them to customers. Is buying directly from a paper cup manufacturer always cheaper? No. Pricing depends on materials, cup structure, coating, printing, quantity, packaging, customization, shipping terms, and other factors. Buyers should compare the complete quotation rather than only the unit price. Are manufacturers better for custom paper cup orders? A manufacturer can provide more direct communication with the production side, which can be useful for custom sizes, printing, coatings, cup structures, packaging, and repeated production. The actual capabilities of each supplier should still be verified. Can a trading company provide customized paper cups? Yes. A trading company can coordinate customized production with a manufacturing factory. Buyers should confirm who is responsible for production, quality control, sample approval, and final specifications. What should I check before ordering paper cups in bulk? Check the material, size, cup structure, coating, printing, MOQ, sample quality, production lead time, certifications, packaging, shipping terms, and quality control procedures. Can ElementsCup supply products besides paper cups? Yes. Elements Packaging's current product range includes paper cups, paper lids, paper food boxes, paper bowls, paper trays, paper bags, paper straws, and compostable cutlery.
  • What to Consider When Buying Paper Food Bowls for Restaurants What to Consider When Buying Paper Food Bowls for Restaurants Sep 14, 2026
    Material and lining come first when you buy paper food bowls. These two choices determine whether a bowl handles your specific menu items without failing. The wrong pick leads to leaks, soggy food, customer complaints, and wasted money on bulk orders that sit unused in your storeroom.   Your restaurant needs packaging that performs under real conditions. Every food service industry buyer faces the same challenge: matching the bowl to the food, not the other way around. This guide walks you through a practical decision sequence—material, size, performance, lids, branding, bulk buying, and sustainability—so you can evaluate any supplier or product with confidence. You will learn to ask the right questions before placing that first order.   Key Takeaways Choose the right material and lining for your food. PE lining handles hot foods well. PLA lining works for cold items and is compostable. Match the bowl size to your menu. Use wider bowls for salads and grain bowls. Use deeper bowls for soups. Standard sizes like 12-16 oz save money and reduce waste. Test each bowl with real food before buying in bulk. Check for leaks, heat retention, and lid fit. This prevents problems during delivery. Custom printing promotes your brand. Plan artwork early and allow 6-8 weeks for production. Buy in bulk to save money and ensure consistent quality. Compostable bowls are great for cold foods. They cost more than PE-lined bowls. Check local composting facilities to make sure they are accepted.   Start With Material and Lining Your decision on paper food bowls begins with material and lining. These two Elements control heat, moisture, and grease performance. Common base materials include: Standard paper — lightweight and economical for dry items. Kraft paper — strong and durable for heavier foods. Bamboo paper — natural appearance with good strength. Cupstock paper — standard for hot and cold cups. Aluminum-laminated paper — excellent insulation for hot liquids. Sugarcane — compostable from renewable fiber.   These base materials form the foundation of your paper packing for food. Standard paper works well for dry snacks and light sides. Kraft paper adds strength for heavier ingredients like grain bowls. Bamboo paper offers a natural aesthetic that appeals to eco-conscious customers. Sugarcane is fully compostable but often requires a PLA lining for moisture resistance. Each option brings different trade-offs in cost, strength, and sustainability.   But the lining inside the bowl does the real work. It creates the barrier between your food and the paper. You need to choose the right lining type first.   PE vs PLA Lining Two lining types dominate the market: PE (polyethylene) and PLA (polylactic acid). PE lining is a plastic coating. It resists moisture, oil, and heat well. But it is not compostable. PLA lining comes from plant starches. It is compostable in industrial facilities. However, it has clear temperature limits. Heat tolerance varies significantly between these two options. The table below shows the maximum heat tolerance for each lining type: Lining Type Maximum Heat Tolerance Suitable for Hot Soup? PE (Polyethylene) Up to ~90–95°C Yes — full range of hot soup service Standard PLA Up to ~55–60°C No — unsuitable for boiling broth CPLA (Crystallized PLA) Up to ~85°C Partially — viable for hot applications at higher cost PE liners withstand temperatures up to 120°C during production. They remain intact around 95°C during critical delivery periods. This makes PE-lined paper bowls a reliable choice for hot soups and stews. In contrast, PLA coatings begin to break down above 85°C. They become unsuitable for boiling liquids. PLA softens at relatively low temperatures and is unsuitable for hot soup. CPLA is crystallized PLA, heat-treated to withstand 90–100°C. Always confirm which type you're ordering — the difference is significant for hot-liquid service. Cost also differs. PLA coating is a newer, more specialized material. It costs roughly 20–30% more per unit than PE. For bulk orders, this price gap adds up quickly. If you serve hot, greasy items daily, PE lining delivers the quality you need at a lower cost. If you want compostable bowls for cold items, PLA is the better choice.   CPLA offers a middle-ground option. It handles higher temperatures than standard PLA but costs more than PE. Consider CPLA if you need hot-food capability with compostable claims.   Reputable suppliers offer both PE and PLA lined paper bowls. You can match the paper bowl lining to your specific menu items. This flexibility helps you control costs without sacrificing performance. Suppliers can also advise on CPLA options for hot applications.   Single-Wall vs. Double-Wall The wall construction of your paper bowl affects insulation and structure. Single-wall bowls use one layer of paper. They work best for cold or dry items like salads, desserts, and sides. Double-wall bowls add a second layer of paper with an air gap. This gap provides insulation, keeping hot foods hot and hands cool.   For hot soups and broth, double-wall construction is essential. It prevents heat transfer to the outer surface. Your customers can hold the bowl comfortably. It also strengthens the bowl structure. This reduces the risk of collapse during delivery.   Single-wall paper bowls cost less. They save on storage space and material. But they cannot handle hot, liquid-heavy meals. Match the wall type to your menu. Use single-wall for sides and cold entrees. Use double-wall for soups, stews, and hot grain bowls.   Your choice of wall construction also affects lid fit. Double-wall bowls have a thicker rim. You need lids designed for that specific wall thickness. Verify compatibility before ordering bulk. Test the lid fit with each wall type during your sample run. A loose lid causes leaks during transport. A tight lid keeps food secure.   Test your wall choice with real menu items. Fill a single-wall bowl with hot soup and watch for softening. Try a double-wall bowl with the same item. The difference in performance becomes clear immediately. Request samples from your supplier and run these tests before placing a large order.   Paper bowls are available in both single-wall and double-wall options. Lids are designed to match each bowl type, ensuring a perfect fit. You can achieve the build quality your menu demands with the right paper bowl. Suppliers can help you select the correct wall thickness for each dish.   Size Paper Bowls for Your Menu Diameter, height, and volume must match your portion size and food type. A bowl that is too small forces you to under-serve. A bowl that is too large makes a normal serving look skimpy. For takeout and delivery, paper bowls commonly range from 8 oz to 24 oz, with 12 to 16 oz being typical for main course items. Within that range, you match the shape and capacity to each menu category.   Grain Bowls, Salads, and Entrees Grain bowls and salads need wider, shallower shapes. A broad surface spreads ingredients evenly and lets customers see the full mix. Soups and broth need the opposite: deeper, narrower shapes that hold heat and reduce spill risk during transport. When you size a takeaway disposable paper bowl for delivery, remember that a full bowl travels worse than a partly filled one. Leave headspace for movement.   Industry data supports standardizing your sizes. Restaurants commonly choose 12–16 oz soup bowls because this range delivers consistency and aligns with global restaurant standards. Standardized sizes in the 12–16 oz range help restaurants balance cost control with customer expectations.   Consistent servings reduce waste and increase satisfaction. A 2024 case study of a U.S. casual dining chain found that switching from oversized 20 oz plastic bowls to standardized 16 oz kraft paper soup bowls cut food waste by 18%, lowered packaging costs by 12%, and drew customer praise for "perfectly sized" portions. For side soups or combo meals, 8 oz is the standard. According to Datainsights Market (2024), 12oz small paper bowls account for over 35% of paper bowl sales globally, making them the most common size for everyday dining, including poke bowls.   Desserts, Sides, and Samples Smaller paper bowls handle desserts, sides, and samples. An 8–16 oz capacity fits a single scoop of ice cream, a side salad, or a dipping portion. These smaller formats also work well for tasting menus and sample flights. You gain portion control and lower your per-unit cost at the same time.   Suppliers offer a range of paper bowl sizes across every menu category. You can source 8 oz bowls for sides and 16 oz bowls for entrees from one supplier. That consistency protects your quality standards across the whole menu.   Test Each Paper Bowl for Heat and Cold Food temperature, moisture level, oil content, portion size, lid design, and expected delivery time all affect how a paper bowl performs. You cannot judge a bowl by looking at it. You must test it with your actual menu items under real conditions. This step separates packaging that works from packaging that fails.   Heat Retention and Condensation Hot items like soup or broth demand strong heat retention and structural strength. A paper bowl that softens under heat will collapse during delivery. You need a bowl that holds its shape from the kitchen to the customer's door. Double-wall construction and PE lining help here. They keep the exterior cool and the interior intact.   Cold items like salads and chilled desserts face a different enemy: condensation. Moisture builds on the exterior surface. This weakens the paper structure over time. A bowl that feels firm at packing may turn soft and unstable within a half hour. You must test for this specifically. Use the following table to plan your condensation trials. Match the test duration to your food type and bowl capacity. Food Condition Main Packaging Concern What to Inspect Trial Duration High-moisture (fruit, whipped cream, pudding) Condensation and sogginess Exterior feel and rim stability 45 minutes Frozen (ice cream, gelato, sorbet) Meltwater accumulation Barrier performance after thawing 45–60 minutes Chilled poke Barrier integrity under condensation exposure Check after 30, 60, and 90 minutes with actual ingredients, dressing, and condensation 30 / 60 / 90 minutes 200–300cc bowls (single scoop gelato, frozen yogurt) Condensation softening 20-minute chilled hold 20 minutes Record your results with a consistent standard. Note any visible seepage, structural collapse, lid release, unacceptable softening, or sauce transfer onto the outside of the pack. These observations tell you whether a paper bowl meets your service standards.   Lid Fit and Leak-Proof Transport Lid compatibility is critical for paper food bowls used in delivery. A lid must snap securely onto the rim. It must stay in place through handling, stacking, and vehicle movement. A loose lid leads to leaks. A leak ruins the meal and damages your brand.   Test lid fit with every paper bowl size you plan to use. Fill each bowl to its normal capacity. Attach the lid. Shake the bowl gently. Turn it on its side. Watch for drips at the rim. Repeat this test after the bowl sits for the expected delivery time. Heat and moisture can change how the lid seals.   Request samples from your supplier before you commit to a bulk order. Run full-menu tests with your actual recipes. Use the same portion size and packaging process your kitchen follows. This reveals problems that a simple visual check cannot catch.   Suppliers provide lid-matched paper bowls and can advise on leak-proof testing. Their team helps you verify that every paper bowl and lid combination meets your quality requirements. You gain confidence before placing a large order.   Brand and Buy in Bulk Custom printing turns your paper bowls into food packaging that markets your restaurant. Every bowl carries your logo and brand colors. This creates branding opportunities with every order. These paper food bowls advertise your brand to every customer.   Custom Printing and Minimum Orders Most suppliers set MOQs for custom-printed paper bowls. You provide artwork files with your logo and chosen colors. The supplier creates a sample for your approval. This sampling stage takes 1–10 days from design file confirmation. After sample approval, production plus shipping runs 3–6 weeks. Larger orders or extra finishing steps extend the timeline further. A safer estimate from design file to finished product is 6–8 weeks. Work with your supplier early to finalize artwork files. This reduces revision time and keeps your timeline on track. Stage Typical Lead Time Sampling from design file confirmation 1–10 days Production after proof approval About 7 business days US delivery 2–5 business days Total estimated lead time About 9–12 business days (roughly 2–2.5 weeks) The total timeline ranges from 2–8 weeks depending on your supplier. Plan your artwork early. Confirm colors with a printed proof before production. This avoids costly reprints.   Inventory and Supplier Vetting Bulk purchasing starts with accurate forecasting. Calculate weekly usage for each paper bowl size you serve. Order enough to cover 8–12 weeks of service. Store inventory in a dry area. Rotate stock by placing older shipments in front. Good inventory management improves your service reliability.   When you vet a paper bowl supplier, run systematic checks. Professional procurement managers use these criteria: Criterion Description Cup stiffness standard Ask for stiffness standard of 95°C hot drink cups upon factory release Color consistency Verify supplier guarantees color consistency across different materials Lid blind buckle test (10 times) Test lid fastening; if it fails 2+ times, mold precision is off Heat sealing test (multi‑temperature zone) Adjust sealer to 160°C, 170°C, 180°C; good cups seal perfectly Stacked compression test Fill with hot soup, stack 3 layers for 30 minutes; pass only if no collapse These tests reveal real quality levels. For food packaging procurement, consistency matters. Run these checks on samples before bulk ordering. A supplier who passes delivers reliable paper bowls.   Suppliers support custom printing and bulk orders for restaurants. Their team helps you plan artwork, meet MOQs, and verify quality. You get branded paper bowl supplier service. Your restaurant benefits from packaging that maintains your standards.   Sustainability in Food Packaging Your customers and local regulators now expect sustainable food packaging. Compostable and recyclable paper bowls answer that demand. You gain a marketing advantage and reduce your environmental footprint at the same time.   Compostable and Recyclable Options Sugarcane, bamboo, and PLA-lined paper bowls are common compostable choices. Each material breaks down in industrial composting facilities. Recyclable paper bowls work well for dry items. You can direct them into standard paper recycling streams. PLA-lined paper bowls carry a clear heat limit. You must respect that limit to avoid failure. PLA has a low heat tolerance. Hot food or direct sunlight can soften and deform it, so it is best reserved for cold items like parfaits, smoothie bowls, and chilled noodle salads. PLA-lined compostable paper bowls typically tolerate temperatures below 50°C. This makes them unsuitable for deep-fried or heavily sauced menu items served hot. Match compostable paper bowls to cold or room-temperature dishes. Use PE-lined paper bowls for hot soups and fried foods.   Balancing Eco-Goals and Budget Compostable options cost more than PE-lined bowls. The table below shows annual costs for a small salad shop using 60,000 bowls per year. Packaging Option Unit Cost (24oz) Annual Bowl Cost Lid Cost Total Packaging Cost PE Basic $0.10 $6,000 $1,800 $7,800 PLA Standard (compostable) $0.13 $7,800 $1,800 $9,600 Water-Based (compostable) $0.16 $9,600 $2,400 $12,000 Switching from PE to PLA Standard adds $1,800 per year. Water-Based compostable options add $4,200 per year. You must weigh these premiums against your sustainability goals.   Match your choices to actual menu items and local composting infrastructure. Check whether your area accepts compostable food packaging. Without proper facilities, compostable paper bowls end up in landfills. That defeats the purpose.   Suppliers offer sustainable food packaging options to help your restaurant meet eco-goals without sacrificing performance. Their team can guide your selection of paper packing for food and takeaway disposable paper bowl products. You get quality you can trust and sustainability you can verify.   Start with material and lining. Then verify these points before you buy: Size matches your portion and menu category. Heat and cold performance holds up in real delivery conditions. Lids snap tight and survive transport. Custom printing fits your brand and budget. Bulk pricing and lead times work for your operation. Sustainability claims match your local infrastructure. Request samples from suppliers. Test every Paper Food Bowl with your actual recipes. Check how each Takeaway Disposable Paper Bowl handles heat, moisture, and movement. Confirm that your Paper packing for food meets your standards before you commit to a large order.   Choosing the right bowl is an operational decision. It affects food quality, customer satisfaction, and your brand image. Treat it like one.   FAQ What is the difference between PE and PLA lining? PE lining resists moisture, oil, and heat well. It is not compostable. PLA lining comes from plant starches and is compostable in industrial facilities. PLA has lower heat tolerance than PE. Choose PE for hot, greasy foods. Choose PLA for cold items when you want compostable Paper packing for food. How do I know which size Takeaway Disposable Paper Bowl fits my menu? Match diameter, height, and volume to your portion size. Use wider, shallower bowls for grain bowls and salads. Use deeper, narrower bowls for soups and broth. Smaller 8–16 oz bowls work for desserts and sides. Test with real servings before ordering bulk. Can I print my restaurant logo on Paper Food Bowls? Yes. Most suppliers offer custom printing with minimum order quantities. You provide artwork files with your logo and colors. The supplier creates a sample for approval. Production and shipping follow. Plan 6–8 weeks from design file to finished product. Confirm colors with a printed proof. How do I test a paper bowl for leaks before buying in bulk? Fill each bowl to normal capacity. Attach the lid. Shake gently and turn it on its side. Watch for drips at the rim. Repeat after the expected delivery time. Heat and moisture can change how the lid seals. Request samples and run full-menu tests with your actual recipes. Are compostable paper bowls suitable for hot foods? Standard PLA-lined compostable bowls tolerate temperatures below 50°C. They work best for cold items like parfaits and chilled salads. CPLA handles higher temperatures but costs more. For hot soups and fried foods, PE-lined bowls deliver reliable performance. Match your choice to actual menu items and local composting infrastructure.
  • The Benefits of Double Wall Paper Coffee Cups for Hot Beverage Delivery The Benefits of Double Wall Paper Coffee Cups for Hot Beverage Delivery Sep 10, 2026
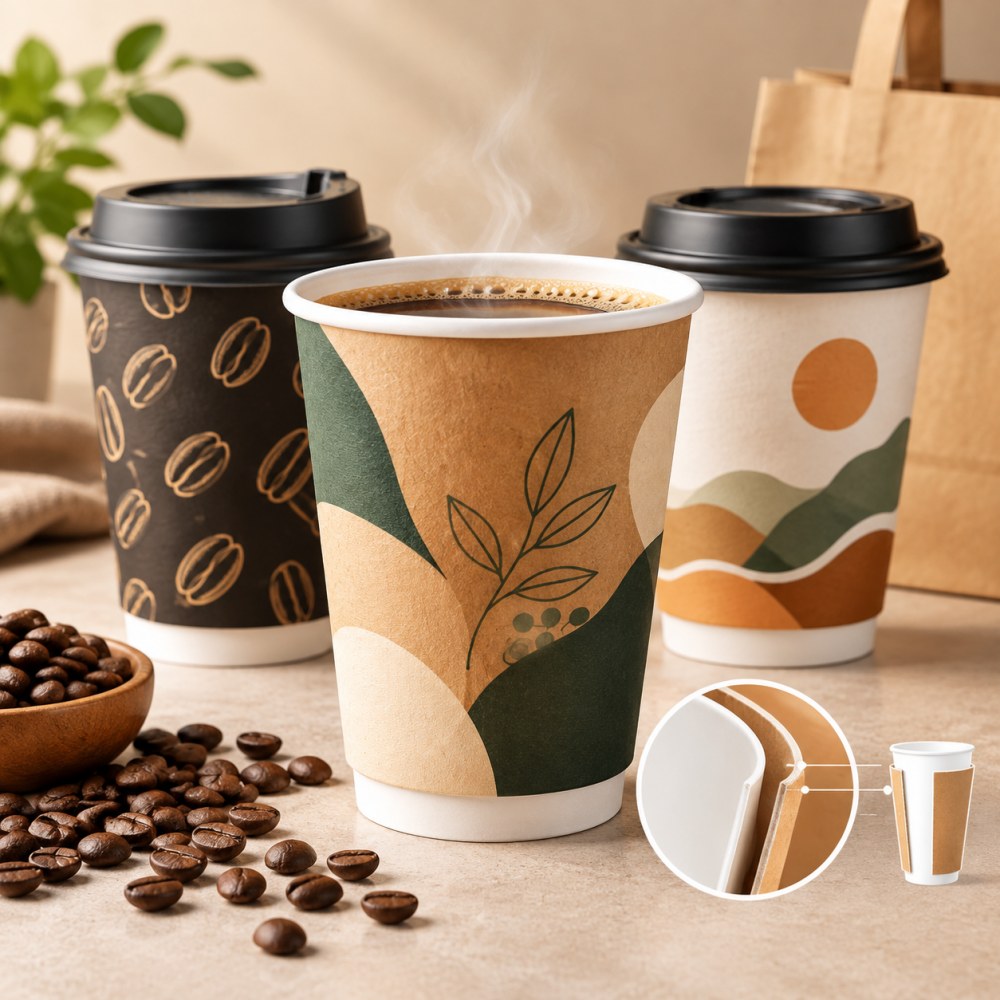
    Hot beverage delivery creates a packaging challenge that coffee shops, cafés, restaurants, catering companies, and food delivery brands must solve every day: how can a cup keep a drink comfortable to hold while maintaining a professional presentation during transportation? Double wall paper coffee cups are designed specifically for this type of application. Their two-layer construction creates an insulating air space between the inner cup and outer layer, helping reduce heat transfer to the consumer's hand while providing a stronger structure for takeaway and delivery service. For wholesale buyers and foodservice packaging distributors, choosing the right double wall cup can improve customer experience, simplify hot beverage delivery, strengthen brand presentation, and support customized packaging programs.   What Is a Double Wall Paper Coffee Cup? A double wall paper coffee cup consists of an inner paper cup combined with an additional outer paper layer. Unlike a conventional single wall cup, the second layer provides additional insulation and structural support. The space between the layers helps reduce direct heat transfer from the beverage to the outside surface. This construction makes double wall cups particularly suitable for coffee, tea, hot chocolate, lattes, cappuccinos, and other hot takeaway beverages. The design is also useful when drinks need to travel from a café or restaurant to a customer's home, office, hotel, event, or workplace. Elements Cup describes its double wall paper cups as food-grade, insulated products that support custom design. Its product range includes different sizes, materials, linings, colors, logos, and packaging configurations for wholesale and customized orders. For businesses looking for a dedicated product range, the double wall paper cups category provides a useful starting point for comparing available styles.   Custom printed double wall paper coffee cups can combine insulation with strong brand visibility.   Why Are Double Wall Cups Better for Hot Beverage Delivery? Hot beverage delivery is different from traditional in-store coffee service. When a customer receives a drink at a café counter, the cup may only need to be carried for a few minutes. Delivery creates a longer handling period and introduces movement, temperature changes, stacking, and transportation conditions. A double wall paper cup addresses several of these challenges at the packaging level. Better hand comfort: The outer wall reduces the amount of heat transferred to the consumer's hand. Improved insulation: The additional layer helps slow heat transfer from the beverage to the external surface. Stronger structure: Two paper layers can create a more rigid cup than a basic single wall construction. Better delivery experience: A sturdy cup can feel more secure when customers receive hot drinks away from the café. Premium appearance: The outer wall creates additional opportunities for high-quality branding and printing. Reduced accessory dependence: In some applications, the integrated outer wall can provide insulation without requiring a separate sleeve. These advantages are especially relevant for coffee brands that depend on takeaway and delivery orders. The cup becomes more than a container; it becomes part of the customer's overall experience with the brand.   Double Wall vs. Single Wall Paper Coffee Cups Single wall paper cups are commonly selected when cost and basic beverage containment are the primary considerations. However, hot drinks can make the external surface of a single wall cup uncomfortable to hold without an additional sleeve. Double wall cups introduce another layer of paper, creating a more insulated structure. This makes them a strong option for hot beverage delivery where hand comfort, rigidity, and presentation are important. Single wall: Lightweight, simple, and often suitable for basic beverage service. Double wall: Better insulation, stronger structure, and a premium takeaway appearance. Ripple wall: Uses a textured outer structure to create insulation and a distinctive tactile appearance. Embossed double wall: Combines double-layer construction with an embossed outer surface for additional texture and grip. The best choice depends on the beverage temperature, delivery distance, brand positioning, packaging budget, and customer expectations.   How Double Wall Construction Improves Hand Comfort One of the most important benefits of a double wall paper coffee cup is improved hand comfort. A hot beverage transfers thermal energy through the inner paper wall toward the outside of the cup. Adding a second wall creates another barrier between the hot liquid and the consumer's hand. This does not mean that the outer surface will remain completely cool. Rather, the additional layer helps reduce the rate and amount of heat reaching the outside surface, making the cup more comfortable to hold during normal use. For delivery businesses, this matters because customers may pick up the beverage immediately after receiving it. A cup that feels too hot can negatively affect the perceived quality of the product, even when the coffee itself is excellent.   Better Protection During Coffee Delivery Delivery packaging needs to handle more movement than an in-store beverage. Cups may be placed inside paper bags, drink carriers, delivery boxes, or insulated bags. They can experience vibration and minor impacts while being transported by car, bicycle, motorcycle, or courier. A rigid double wall structure can provide greater stability during handling. The outer layer adds material around the cup body, which can help the cup maintain its shape when customers grip it or when several drinks are packed together. For commercial buyers, however, cup construction should always be evaluated together with lid fit, rim quality, sealing performance, carton packing, and delivery carrier compatibility. A strong cup alone cannot compensate for an unsuitable lid or poorly designed delivery packaging.   Custom Printing Makes Double Wall Cups a Branding Tool Hot beverage delivery gives brands fewer opportunities to communicate directly with customers than an in-store experience. A customized coffee cup can therefore become an important mobile branding surface. Double wall paper cups offer a relatively large printable exterior area. Coffee shops can use this space for logos, brand colors, slogans, seasonal artwork, QR codes, social media information, or promotional messages. For wholesale and private label buyers, customized printing can also help create a consistent packaging system across multiple beverage sizes. Instead of using generic disposable cups, a brand can develop a recognizable visual identity that appears across delivery orders, takeaway counters, events, and catering services.   Full-color custom printing helps takeaway coffee brands turn disposable cups into mobile marketing assets.   What Sizes Are Available for Hot Beverage Delivery? Cup size should be selected according to the beverage menu rather than choosing a size simply because it is popular. A coffee shop may need several capacities for espresso-based drinks, regular coffee, tea, hot chocolate, and specialty beverages. Elements Cup's custom double wall hot cup specification lists sizes including 7 oz, 8 oz, 8 oz squat, 10 oz squat, 12 oz, 16 oz, 16 oz squat, and 20 oz. This range allows buyers to develop packaging for different menu categories and serving volumes. For example, an 8 oz cup can work well for smaller hot beverages, while 12 oz and 16 oz sizes are commonly useful for standard takeaway coffee programs. Larger sizes can support bigger specialty drinks or extra-volume beverage menus. Before ordering in bulk, buyers should test the selected cup with the actual beverage recipe, lid, carrier, and delivery bag to ensure the complete packaging system works together.   Choose the Right Paper and Inner Lining The paper structure is only one part of a commercial coffee cup. The inner lining also plays an important role because it helps the cup resist moisture and prevents the beverage from penetrating the paper structure. Depending on the product specification and market requirements, buyers may consider conventional PE lining, PLA lining, or aqueous barrier coating. Each option should be evaluated according to performance requirements, environmental claims, local regulations, disposal infrastructure, and certification needs. Elements Cup lists bamboo fiber, kraft paper, and plain white paper as material options for its double wall hot cups, with PE, PLA, and aqueous barrier options available for the lining. The company also lists customization of size, color, logo, lining, and packaging. For buyers prioritizing alternative coating solutions, a dedicated compostable PLA cup range can be considered as part of a broader sustainable packaging strategy.   Double Wall Cups and Sustainable Packaging Sustainability is increasingly important for foodservice packaging buyers, but environmental claims should always be evaluated carefully. A paper cup is not automatically compostable or recyclable simply because its main structure is made from paper. The coating, adhesives, printing inks, packaging configuration, local waste infrastructure, and applicable certification standards can all affect the end-of-life pathway. For example, Elements Cup offers different barrier coating choices, including PLA and water-based aqueous coatings. Its product information notes that PLA and aqueous barrier options can support different compostability pathways depending on the specific product and applicable conditions. For B2B buyers, the most reliable approach is to ask the manufacturer for the exact material specification and relevant certification for the product being ordered, rather than relying on broad terms such as “eco-friendly” or “biodegradable.”   Why Double Wall Cups Work Well for Coffee Shops and Delivery Brands For coffee shops, cafés, bakeries, restaurants, hotels, catering companies, and beverage delivery platforms, double wall cups can provide several business benefits at the same time. Improved customer comfort: Customers can handle hot drinks more comfortably. Professional presentation: A well-designed cup can reinforce the quality of the beverage. Brand visibility: Custom printing keeps the brand visible during takeaway and delivery. Operational simplicity: An integrated double wall may reduce the need for separate cup sleeves in suitable applications. Product differentiation: Custom sizes, colors, printing, and coatings help brands develop a more distinctive packaging system. Wholesale scalability: Standardized specifications make it easier to plan recurring bulk orders.   Branded double wall cups can create a clean and recognizable appearance for takeaway coffee programs.   When Should You Choose Ripple Wall or Embossed Wall Cups? Double wall construction is not the only way to improve insulation and handling. Ripple wall and embossed wall cups can provide different combinations of grip, texture, insulation, and visual appeal. Ripple wall cups use a textured outer layer that creates air pockets and gives the cup a distinctive tactile surface. They can be particularly attractive for cafés that want a more premium or handcrafted appearance. Embossed double wall cups can provide a similar combination of insulation and texture while creating additional opportunities for visual differentiation. They may be worth considering when the packaging itself is part of a brand's design strategy. For businesses comparing these structures, Elements Cup's paper cup collection includes double wall, ripple wall, embossed wall, single wall, and other paper cup solutions.   How to Select Double Wall Coffee Cups for Wholesale Ordering Wholesale buyers should evaluate more than the unit price when selecting a cup supplier. A lower initial quotation may not provide the best total value if the product has inconsistent dimensions, poor printing quality, weak carton packing, or unreliable delivery times. Key questions to ask your paper cup manufacturer: What cup sizes and capacities are available? Which paper materials can be used? What coating options are available? Can the cup be fully customized with a brand logo? What printing method and color specifications are supported? What is the minimum order quantity? Can the supplier provide pre-production samples? What certifications are available for the selected material? How are cups packed for international shipping? Can the manufacturer provide matching lids and beverage accessories? Elements Cup's published double wall cup specification lists an MOQ of 50,000 pieces, a stated lead time of approximately 30 days, and customization for size, color, logo, lining, and packaging. Actual commercial terms should be confirmed with the supplier based on the final specification and order requirements.   Pair Double Wall Coffee Cups With the Right Lids A cup and lid should be treated as one packaging system. During hot beverage delivery, the lid needs to fit securely, resist spills, and match the cup rim accurately. An unsuitable lid can create leakage problems even when the cup itself performs well. For coffee delivery programs, buyers should test the complete combination of cup, lid, beverage temperature, carrier, and delivery bag before committing to a large production order. Elements Cup also supplies cup accessories, including lids, cup holders, sleeves, and straws, allowing buyers to source complementary foodservice packaging from the same supplier.   How Double Wall Paper Cups Support a Better Delivery Experience The success of hot beverage delivery depends on more than keeping coffee inside a container. Customers notice whether the cup feels comfortable, whether the lid stays secure, whether the packaging looks professional, and whether the beverage arrives in a condition that matches their expectations. Double wall paper coffee cups address several of these requirements through their structure. The additional paper layer helps provide insulation, rigidity, and a larger surface for customized branding. Combined with the correct lid and delivery carrier, they can form a practical packaging solution for modern takeaway and delivery businesses. For brands that serve large volumes of coffee and other hot beverages, selecting the right cup construction at the beginning can also make procurement more consistent. Standardized sizes, materials, printing specifications, and packaging configurations can simplify repeat purchasing as the business grows.   Final Thoughts for Wholesale Buyers Double wall paper coffee cups are a strong option for hot beverage delivery because they combine insulation, structural strength, consumer comfort, and branding potential in one packaging format. They are especially useful for coffee shops, cafés, restaurants, catering companies, foodservice distributors, and beverage brands that depend on takeaway and delivery sales. When selecting a supplier, look beyond the appearance of the cup. Evaluate the paper material, inner coating, cup size, printing quality, lid compatibility, certifications, MOQ, production capacity, packaging, and export experience. Looking for custom double wall paper coffee cups for your beverage business? Start by defining your cup size, beverage type, printing requirements, coating preference, lid specification, and expected order volume. Then request samples and test the complete packaging system under real delivery conditions. With the right specification and a reliable manufacturing partner, custom double wall paper cups can help your business deliver hot beverages more comfortably while turning every takeaway order into an opportunity for stronger brand recognition.  
  • Double Wall Paper Cups: B2B Engineering, Coatings & Sourcing Guide Double Wall Paper Cups: B2B Engineering, Coatings & Sourcing Guide Sep 02, 2026
    In today’s commercial food service and specialty coffee landscapes, single-use drinkware is no longer viewed merely as a recurring consumable line item. Instead, it serves as an indispensable physical touchpoint that dictates beverage temperature preservation, consumer tactile comfort, branding longevity, and regulatory environmental compliance. While the historical default for hot beverage service relied on single wall paper cups paired with external corrugated sleeves, global quick-service restaurant (QSR) chains and beverage distributors are aggressively shifting toward precision-manufactured double wall paper cups produced by specialized manufacturers like Elements Packaging.   This architectural migration is fueled by both physical performance and enterprise unit economics. The friction of warehousing, unboxing, and manually assembling paper sleeves during peak barista workflow creates notable labor constraints and throughput bottlenecks. Concurrently, tightening packaging regulations across North America and Europe—such as the European Union Single-Use Plastics Directive (SUPD) and expanding per- and polyfluoroalkyl substances (PFAS) restrictions—compel procurement teams to thoroughly assess substrate board grammage, liner chemistry, and circular lifecycle economics before committing to multi-container purchase contracts.   Key Takeaways Thermal air insulation: The engineered dead-air pocket eliminates the need for external paper sleeves while keeping outer grip temperatures below 46°C. Sustainable barrier options: Aqueous dispersion coatings provide certified repulpability in standard curbside paper recycling streams without plastic sorting hurdles. Total cost advantage: Integrated double wall vessels reduce overall operation costs by removing secondary sleeve inventory, freight, and barista assembly delays. Standardized lid fit: A universal 90 mm rim diameter accommodates 12 oz, 16 oz, and 20 oz sizes, consolidating lid inventory across multiple drink formats. Verified factory testing: High-speed automated filling lines require strict 24-hour ultrasonic seam hydrostatic sealing and PFAS-free food contact certification. This engineering-driven sourcing manual provides commercial buyers, product packaging engineers, and wholesale importers with a comprehensive assessment of thermal air barrier physics, a comparative matrix of lining polymer chemistries (conventional PE versus plant-based PLA versus repulpable aqueous coatings), realistic Total Cost of Ownership (TCO) models, and critical quality control parameters engineered into production lines at Elements Packaging. Thermal Physics: Micro-Air Gaps and Heat Dissipation Mechanics To understand the mechanical superiority of an engineered double wall cup, one must evaluate heat transfer dynamics across conductive, convective, and radiative channels. In a standard single wall cup, hot liquids poured at temperatures between 85°C and 93°C (185°F - 200°F) establish an instantaneous conductive thermal pathway directly across the single layer of cellulose paperboard. Because wood pulp paper possesses a thermal conductivity coefficient (κ) of roughly 0.05 to 0.08 W/(m·K), thermal energy penetrates the wall within 3 to 5 seconds, causing outer surface temperatures to quickly breach the human dermal pain threshold of 48°C to 50°C (118°F - 122°F). The Insulating Micro-Air Cavity A double wall cup completely arrests this rapid conduction path by nesting an inner paper cup inside an outer wrapped sleeve, creating a calibrated dead-air pocket between 0.5 mm and 1.5 mm wide. Dry, stagnant air is one of the most effective natural thermal insulators, demonstrating a very low thermal conductivity of approximately 0.026 W/(m·K). Because this enclosed clearance is engineered to stay below the critical Rayleigh number threshold, internal natural air convection is suppressed. The technical outcomes include: Exterior Dermal Protection: While the beverage core stays piping hot above 75°C, the cup's exterior grip surface remains within a comfortable 40°C to 46°C window, providing a pleasant handheld experience without burns or hand fatigue. Extended Temperature Retention: Thermal decay curves demonstrate that a sealed double wall paper cup preserves serving temperatures 30% to 35% longer over 45 to 60 minutes compared to un-sleeved single wall paperware. Dual-Use Condensation Defense: For cold applications (iced espresso drinks, cold brew, and frozen smoothies), the same thermal gap prevents the exterior shell from falling below the ambient dew point, eliminating moisture condensation that weakens paper fibers and softens cup rims. Paperboard Grammage (GSM) Matrix & Mechanical Rigidity A frequent complaint from drive-thru operators is cup buckling—where a customer grips the cup body and the sidewall collapses inward, dislodging the lid and spilling boiling liquid. Structural rigidity is determined by the combined basis weight (measured in grams per square meter, or GSM) of the primary virgin board and outer wrap. Below is the industrial standard engineering matrix utilized in commercial-grade manufacturing at Elements Packaging: Cup Size Inner Layer Baseboard Outer Sleeve Board Total Grammage Radial Force Tolerance 8 oz (240 ml) 260 gsm + 18g coating 250 gsm Virgin Kraft/White ~528 gsm < 3.0 mm deflection @ 15 N 12 oz (350 ml) 280 gsm + 18g coating 280 gsm Virgin Kraft/White ~578 gsm < 3.2 mm deflection @ 18 N 16 oz (480 ml) 300 gsm + 20g coating 300 gsm Virgin Kraft/White ~620 gsm < 3.5 mm deflection @ 20 N 20 oz / 22 oz (650 ml) 320 gsm + 20g coating 320 gsm Virgin Kraft/White ~660 gsm < 3.8 mm deflection @ 22 N Inner Barrier Chemistry: PE vs. PLA vs. Aqueous Dispersion Coatings Cellulose fibers are naturally hydrophilic. Without an impermeable inner barrier coating, aqueous liquids, coffee lipids, and acidic beverage compounds penetrate the paper matrix, triggering delamination and structural wall collapse within minutes. As environmental legislation reshapes market access across Europe, Australasia, and North America, selecting the proper internal liner is one of the most consequential decisions for packaging buyers. Conventional Polyethylene (LDPE) Extrusion Low-Density Polyethylene remains the historical benchmark for moisture-barrier performance. Melt-extruded onto virgin board at thicknesses between 15 μm and 22 μm, LDPE forms a reliable, cost-effective seal that withstands boiling water up to 105°C. However, because the plastic film adheres tenaciously to the cellulose substrate, standard municipal hydropulping recycling facilities cannot easily segregate the fibers, causing most LDPE-lined cups to end up in landfills or waste-to-energy incinerators. Polylactic Acid (PLA) Biopolymers Polylactic Acid is derived from plant dextrose sources, including fermented corn starch and sugarcane. PLA offers heat and moisture resistance comparable to polyethylene while meeting industrial compostability standards (EN 13432 and ASTM D6400). Under controlled industrial composting conditions (58°C - 65°C and 60% humidity), PLA-lined paper cups biodegrade into water, carbon dioxide, and organic biomass within 90 to 180 days. Buyers should verify that suppliers utilize heat-resistant, crystallized PLA formulations, as early generation PLA could soften when exposed to prolonged 90°C+ drip brew coffee. Next-Generation Aqueous Dispersion Coating (Water-Based Barrier) Aqueous coatings represent the most significant technological leap in paper cup manufacturing. Rather than extruding a continuous extruded plastic film, an aqueous polymer emulsion is applied to the paper web via flexographic or gravure roller coaters and subsequently heat-cured. This yields an ultra-thin barrier layer (5 to 9 gsm) that prevents moisture and oil transmission. Crucially, aqueous-coated cups are 100% repulpable and curbside recyclable within conventional paper recycling streams (verified under Western Michigan University or PTS-RH 021/97 protocols). When submerged in standard papermaking hydropulpers, the water-based coating disperses without clogging filtration screens or yielding microplastic remnants, allowing the underlying virgin cellulose pulp to achieve recovery rates in excess of 92%. Technical Attribute PE Lamination PLA Biopolymer Aqueous Dispersion Primary Feedstock Petroleum based Bio-renewable plant starch Water-borne acrylic polymer Maximum Fluid Temp Up to 105°C (221°F) Up to 92°C - 95°C Up to 100°C (212°F) End-of-Life Destination Landfill / Waste-to-Energy Industrial Composting Facility Standard Curbside Paper Bin EU SUPD Marking Mandate Mandatory "Plastic" turtle logo Mandatory "Plastic" turtle logo Exempt in specific jurisdictions Commercial Cost Index Baseline (1.00) +18% to +25% +12% to +18% TCO Procurement Modeling: Integrated Double Wall vs. Single Wall + Sleeve A common pitfall among inexperienced purchasing agents is comparing itemized unit costs in isolation. While an unprinted single wall paper cup may carry an FOB price 30% lower than an integrated double wall cup, evaluating the operational Total Cost of Ownership (TCO) paints a dramatically different picture. The Hidden Supply Chain Costs of Auxiliary Sleeving Dual Inventory Management & Stockout Risk: Procuring cups and sleeves separately requires managing two distinct vendor supply chains, two purchase orders, separate freight rates, and independent storage allocations. If paper sleeves experience stockouts, store associates instinctively "double-cup" (nesting two single wall cups together), immediately inflating unit packaging cost by 100%. Barista Speed of Service Bottlenecks: Motion-study data reveals that reaching for, expanding, and sliding an embossed sleeve onto a hot cup consumes 2.5 to 4.0 seconds per transaction. In a busy drive-thru location serving 1,000 hot beverages daily, this represents nearly an hour of diverted barista labor each day, slowing queue velocity and reducing peak revenue capacity. Workstation Clutter & Brand Concealment: Auxiliary sleeves require dedicated countertop dispensers, consuming precious workspace next to espresso machines. Furthermore, standard sleeves cover up to 55% of the cup surface, concealing custom promotional artwork or brand logos printed on the base cup. Outer Surface Architectures: Smooth vs. Embossed vs. Ripple Wall The outer wrap of a double wall cup can be formed in multiple configurations depending on specific branding, tactile grip, and thermal performance demands: Smooth Double Wall Cups The smooth configuration pairs an inner container with a flat exterior paper wrap. This format offers an ideal surface for photographic flexographic or high-precision offset printing. Brands seeking crisp multi-color halftones, full-wrap CMYK imagery, matte soft-touch coatings, or metallic foil stamping typically favor smooth double wall cups for maximum graphic fidelity. Embossed Double Wall Cups Embossed cups pass the outer wrap through specialized mechanical stamping rollers before adhering it to the inner cup. This creates dimensional textures—such as diamond grids, honeycomb patterns, or custom brand badges—that elevate the tactile experience while reducing hand contact area by over 35%. The structural air chambers between fingers and paper deliver exceptional thermal protection without the heavier weight of corrugation. Ripple (Corrugated) Wall Cups Ripple wall cups feature an external fluted S-curve or vertical corrugated layer. By creating substantial physical separation between the inner hot cup and the outer grip surface, ripple cups provide maximum insulation for near-boiling beverages like pour-over teas and broths. They are widely recognized for their rugged grip and rustic kraft appearance. Factory Quality Assurance Protocols & International Compliance When procuring disposable cups from offshore manufacturers, packaging buyers must implement rigorous incoming quality standards. A defective batch with rim deviations or seam pinholes can result in customer burns, drive-thru spills, and severe brand liability. Commercial production at Elements Packaging complies with verifiable factory testing across three key categories: Ultrasonic Bottom Seam Hydrostatic Testing The bottom knurled seal is the most vulnerability-prone element of any paper cup. Modern production lines utilize ultrasonic welding or high-frequency heating tools to bind the base disc to the sidewall. Quality assurance audits should require standardized dyestuff penetration testing: cups are filled with 90°C methylene blue dye solution and rested on absorbent white paper for a minimum of 4 hours (with rigorous commercial specifications mandating 24-hour zero-wicking stability). Rim Curl Ovality & Automated Lid Compatibility An improperly curled top rim leads to loose lid engagement, liquid leaks, and denesting jams in automated dispensing machines. Tight manufacturing tolerances must maintain rim roundness and bead diameter within ±0.25 mm across production runs. Advanced factories employ integrated optical machine vision systems directly on the packaging conveyor to inspect rim geometry before carton loading. Regulatory Compliance & Chemical Safety Ensure the manufacturing facility holds current, accredited laboratory test certificates verifying the following international standards: US FDA 21 CFR 176.170 / 176.180: Safe contact requirements for aqueous and fatty food substances. EU Framework Regulation (EC) No 1935/2004: Demonstrating total and specific migration thresholds (OML ≤ 10 mg/dm²) in 10% ethanol, 3% acetic acid, and vegetable oil food simulants. PFAS-Free Certification: Laboratory confirmation of Total Organic Fluorine (TOF) < 50 ppm, ensuring full adherence to emerging global chemical safety laws. FSC® Chain of Custody: Verifying raw cellulose paperboard originates from sustainably harvested, certified forests. Ocean Logistics and Container Volume Optimization From a logistical perspective, double wall cups feature a slightly deeper nesting pitch than single wall cups due to the added thickness of the outer wrap. While single wall cups typically nest at 6 mm to 8 mm per cup, double wall cups average a nesting height of 10 mm to 14 mm. This difference affects container utilization: A standard 40ft High Cube (40HC) container typically accommodates between 550,000 and 650,000 double wall cups (packed 500 units per carton; 20 poly-sleeves × 25 cups), compared to approximately 950,000 single wall cups. Savvy supply chain directors offset this ocean freight difference against the complete elimination of sleeve procurement, separate freight charges, and double-cupping inventory losses. Strategic Procurement Checklist for B2B Importers Standardize Universal 90 mm Calibers: Ensure that 12 oz, 16 oz, and 20 oz cups share an identical 90 mm rim diameter, allowing one lid SKU to fit all medium and large hot drinks. Require Water-Based Inks: Mandate food-grade, odor-free water-based flexographic inks to prevent VOC odor migration from compromising delicate espresso crema. Verify Hot-Liquid Load Deflection: Request 95°C hot water sidewall radial compression test reports to guarantee cups remain firm during handover. Demand Reinforced Master Packaging: Specify 5-ply export corrugated cartons with moisture-resistant inner poly bags and corner pallet protection to prevent crushing during ocean transit. Frequently Asked Questions What is the minimum order quantity for custom-printed double wall cups? Commercial custom-printed runs at Elements Packaging generally begin at 50,000 units per artwork SKU for flexographic rotary printing. This threshold ensures full setup amortisation across printing plates, die-cutting tooling, and automated inline outer sleeve laminating stations. Can a single lid size fit multiple capacities of double wall paper cups? Yes. Standardised factory tooling produces 12 oz, 16 oz, and 20 oz double wall cups with an identical outer top rim diameter of 90 mm (±0.25 mm). This allows beverage operations to stock a single lid SKU across all medium and large hot drink formats, cutting storage needs and barista sorting errors. Are aqueous-coated double wall cups genuinely plastic-free and curbside recyclable? Yes. Aqueous dispersion barrier coatings use a water-borne polymer emulsion rather than an extruded solid plastic film (such as PE or PLA). When processed in standard paper pulping systems, the micro-dispersion breaks down cleanly without clogging sieves or producing micro-plastics, achieving certified repulpability rates above 92%. Can double wall paper cups be safely microwaved? Cups featuring water-based aqueous coatings or standard PE liners can safely handle brief reheating intervals (under 60 seconds). However, PLA-lined bio-cups should never be microwaved, as commercial bioplastics begin thermal glass-transition deformation above 60°C, which compromises wall integrity. How does double wall construction perform with cold and iced drinks? The micro-air layer functions bidirectionally. For iced drinks, cold brew, and smoothies, the exterior paper jacket stays above the room-temperature dew point, preventing surface condensation. This keeps the cup rigid and prevents moisture rings on tabletops.
  • Paper Bowls vs Plastic: Why Eco-Friendly Options Win Paper Bowls vs Plastic: Why Eco-Friendly Options Win Aug 28, 2026
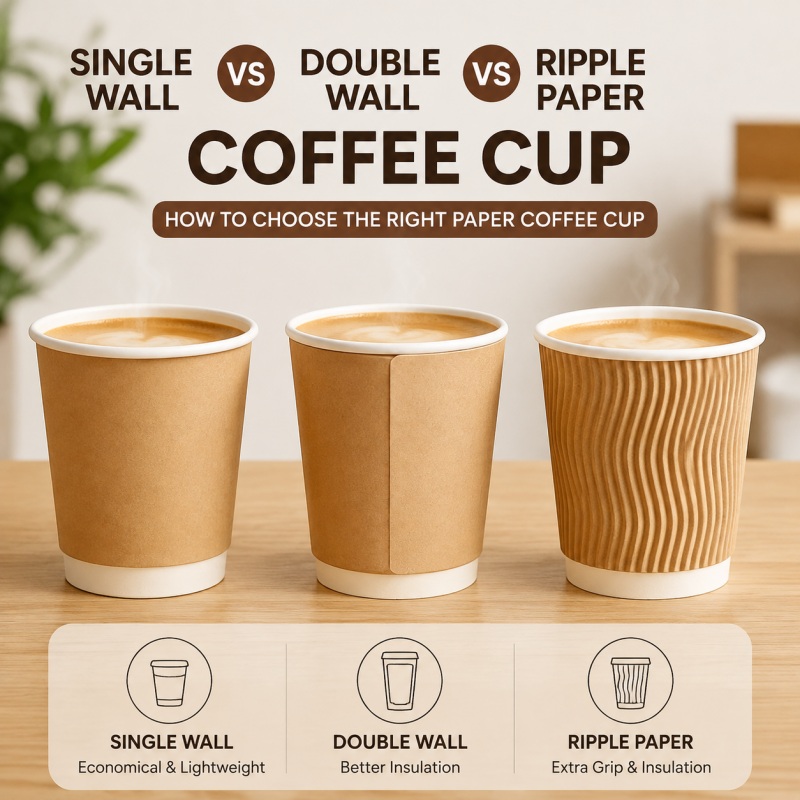
    Every year, billions of plastic bowls end up in landfills and oceans. You might not realize that producing plastic bowls generates roughly double the carbon emissions of paper alternatives—9.7 to 11.3 kg CO2 versus 4 to 6 kg per kilogram of material. The choice matters more than you think. Eco-friendly disposable paper bowls offer a superior solution. You'll discover how they compare across four key dimensions: environmental impact, performance, end-of-life options, and practical cost. Compostable paper bowls break down naturally instead of persisting for centuries. By the end, you'll know exactly how to select sustainable tableware that protects the planet without sacrificing quality. Your next purchase can make a real difference.   Key Takeaways Plastic bowls harm the planet. They come from fossil fuels and take centuries to break down. Paper bowls use renewable materials. They break down in months, not years. Paper bowls handle hot food well. They resist heat and leaks just like plastic. Choose PFAS-free and BPA-free bowls. These are safer for your health. Buy in bulk to save money. Eco-friendly bowls can cost less over time.   Environmental Impact of Disposable Paper Bowls The Problem with Plastic Bowls Plastic bowls trace their origins to a deeply flawed starting point. Nearly all plastics—99 percent—come from fossil fuels like oil, gas, and coal. You might not realize that extracting these resources releases greenhouse gases before manufacturing even begins. The refining process demands intense heat and chemical processing, consuming two to three times more energy than paper production. This energy hunger translates directly into carbon emissions. The pollution crisis extends far beyond production. Plastic bowls take 400 to 1,000 years to degrade in landfills. During that time, they fragment into microplastics that contaminate soil and water. These tiny particles enter the food chain, affecting wildlife and potentially human health. Landfills overflow with single-use plastics that never truly disappear—they simply break into smaller, more dangerous pieces. Global regulations now reflect this urgency. The European Union's SUP Directive banned expanded polystyrene in 2021. Canada followed with a federal ban on PS and PET foodservice items in 2023. Several U.S. states, including California and New York, enforce plastic taxes and bans. Singapore will tax plastic packaging starting in 2025. Australia's state-based bans now cover foam and plastic containers. These policies signal a clear direction: plastic's dominance is ending. "With fossil-fuel-based plastic under global scrutiny, brands that proactively switch to verifiably compostable packaging—like kraft bowls—are not just eco-friendly, they're future-proofing." — Dr. Lara Kim, Environmental Packaging Policy Consultant, Berlin   Renewable Materials for Paper Bowls Eco-friendly disposable paper bowls offer a fundamentally different story. Manufacturers craft them from renewable sources like sugarcane bagasse, bamboo, palm leaf, and recycled paper. Sugarcane bagasse, the fibrous residue after juice extraction, would otherwise become agricultural waste. Bamboo grows rapidly without pesticides. Palm leaves fall naturally from trees. These materials absorb CO₂ during their growth cycle, offsetting emissions during decomposition. The lifecycle comparison reveals stark differences. Kraft paper bowls source from FSC-certified trees or recycled content, absorbing carbon as trees grow. Manufacturing requires lower temperatures and less energy. Transport becomes more efficient because paper bowls nest and weigh less. At end-of-life, compostable paper bowls break down within 60 to 90 days in proper facilities. Plastic bowls persist for centuries. Carbon footprint data confirms the advantage. A bagasse clamshell box weighing 20 grams produces 45 kg CO2e per 1,000 units, saving 60 kg CO2e compared to plastic. A 21-gram burger box generates 48 kg CO2e per 1,000 units, saving 63 kg CO2e. Each kilogram of bagasse replacing polypropylene saves approximately 3.0 kg CO2e. While these figures cover similar bagasse products, the identical material and production process make them representative for bowls. You should look for specific certifications when choosing products. BPI certification verifies genuine compostability. Select unbleached options without PFAS coatings. These chemicals, used for grease resistance, persist in the environment and pose health risks. Unbleached kraft paper avoids chlorine bleaching byproducts entirely. The full lifecycle tells a compelling story. Plastic generates up to 2.5 times more CO₂ than kraft paper across production, transport, and disposal. Custom disposable paper bowls from renewable sources reduce your environmental footprint while meeting the same functional needs. The choice between materials becomes clear when you examine the complete picture.   Performance of Disposable Paper Bowls vs. Plastic Heat Resistance and Leak-Proofing You need bowls that handle real meals—hot soups, oily curries, saucy noodles. Plastic bowls warp under high heat and can leach chemicals into your food. Eco-friendly alternatives perform better than you might expect. Bagasse bowls withstand hot foods up to 220°F (approximately 104°C) without warping or leaking. That temperature covers boiling water and most freshly cooked dishes. Bamboo bowls perform even better in side-by-side testing. At 90°C, bamboo bowls resist warping for 60 minutes with a leakage rate of just 1 percent. Bagasse bowls hold their shape for 45 minutes with a leakage rate under 2 percent. Users rate bamboo bowls 8.9 out of 10 for comfort, while bagasse scores 8.4. These materials deliver strength that plastic cannot match. Microwave and freezer performance varies by bowl type. The table below summarizes what you should expect: Bowl Type Microwave Performance Key Limitation Single-Wall PE-Lined Limited use Liner softening or edge warping Double-Wall Insulated Good when certified Steam buildup if tightly covered Kraft Paper Good when microwave-rated Coating and ink variation PLA-Coated Use with caution PLA may soften at higher heat Bagasse Sugarcane Fiber Generally strong when certified Formula and PFAS status vary You should always check the certification label before microwaving any bowl. Look for explicit microwave-safe claims from the manufacturer. For freezer storage, most compostable paper bowls handle cold temperatures without cracking. Plastic bowls become brittle in freezing conditions, while fiber-based materials maintain their integrity.   Choosing Safe Materials: PFAS-Free and BPA-Free The materials touching your food matter for your health. Many disposable bowls contain PFAS—per- and polyfluoroalkyl substances—added for grease resistance. These chemicals persist in your body and the environment. A consortium of scientists published a new scientific statement in 2020 highlighting serious health concerns linked to PFAS exposure from food packaging: Cancer Hormone disruption Liver and kidney toxicity Harm to the immune system, including decreased response to vaccines Reproductive and developmental toxicity Recent decades of research link PFAS exposure to immune system suppression, lower birth weight, and increased risk for some cancers. These compounds appear in burger wrappers and salad bowls alike. You cannot see them or taste them, but they accumulate in your body over time. BPA presents another concern. This chemical appears in some plastic linings and can mimic estrogen in your body. Even small amounts may disrupt your endocrine system. You should avoid bowls containing BPA entirely. Your safest choice is unbleached, PFAS-free, and BPA-free options. Unbleached kraft paper avoids chlorine bleaching byproducts. PFAS-free coatings use plant-based alternatives like PLA or natural wax. These materials provide grease resistance without toxic persistence. Reputable manufacturers offer bowls that meet these strict safety standards. Some products carry explicit PFAS-free and BPA-free certifications, so you do not need to guess about what touches your food. When you select disposable paper bowls, read the fine print. Look for third-party certifications that verify safety claims. Avoid vague terms like "eco-friendly" without supporting documentation. Your health depends on these details. The performance of these bowls matches or exceeds plastic in everyday use, without the chemical risks. You get strength, heat resistance, and peace of mind in one package.   Compostability and Recyclability of Paper Bowls Compostability Standards and Certifications You see the word "biodegradable" on many products. It does not mean what you think. Any material can eventually break down. "Compostable" carries a specific, verified meaning. A compostable product must decompose into non-toxic components. This happens within a specific timeframe. The process requires controlled conditions. BPI certification sets this standard in the United States. BPI certification confirms that a product meets these requirements. You should look for the BPI logo on disposable paper bowls. Only then can you assume they are compostable. Most compostable paper bowls require industrial composting facilities. These facilities maintain high temperatures and controlled humidity. The conditions accelerate decomposition. Your backyard compost bin rarely reaches these conditions. Bagasse or bamboo fiber bowls break down within 60 to 90 days in an industrial facility. Without access to such a facility, the bowl ends up in a landfill. It cannot decompose there. You should check the label for "industrially compostable" or "home compostable". This tells you what your local setup can handle. Plastic-coated bowls cannot enter compost streams. Even PLA linings cause problems.   Recycling Challenges and Best Practices Recycling paper bowls presents more problems than you expect. Most bowls touch food. Food residue contaminates the recycling stream. A single greasy bowl can ruin an entire batch of recyclable paper. Many bowls also contain plastic linings. Recycling facilities cannot separate PE or PLA easily. These challenges mean most paper bowls never get recycled. Composting offers a much better solution. You can follow a few best practices. First, check the label for certifications like BPI Certified Compostable. Second, scrape all leftover food from the bowl. Third, give the bowl a quick rinse. This removes sauces or oils that slow down composting. Fourth, verify that your local composting facility accepts compostable paper bowls. Not all facilities do. Fifth, send the bowl to an industrial compost facility. Look for the "home compostable" label if you plan to use your backyard bin. Finally, place plastic-coated bowls in the trash. This avoids contaminating compost streams. These steps ensure your efforts actually help the environment.   Practical Considerations: Cost and Availability Cost Comparison: Paper vs. Plastic The assumption that eco-friendly options always cost more deserves closer examination. When you compare bulk pricing, the gap narrows significantly. Standard plastic bowls run $0.05 to $0.10 per unit. Eco-certified paper bowls, whether PLA-coated or bagasse-based, cost $0.20 to $0.50 per unit. That difference ranges from $0.10 to $0.45 per bowl, with a midpoint around $0.275. That per-unit gap tells only part of the story. Quality paper bowls deliver long-term savings through improved durability and reduced waste. Some businesses report reduced waste management costs after switching to biodegradable options. Switching to biodegradable disposable products can reduce waste. Biodegradable paper bowls decompose within 60 to 90 days, while plastic persists for centuries. You avoid the hidden costs of landfill fees and environmental cleanup. Bulk purchasing further offsets the initial price difference. Many suppliers offer competitive pricing for volume orders. When you factor in disposal costs, regulatory compliance, and customer loyalty, the total cost of ownership favors paper.   Where to Find Quality Eco-Friendly Options The market for compostable tableware has expanded dramatically. Industry projections show the Pulp and Paper substrate segment capturing 66.7% of the biodegradable tableware market by 2026. This growth stems from regional legislation targeting polystyrene containers. Distributors now stock certified compostable alternatives to meet demand. Trend Data: 68% of quick-serve restaurants plan to phase out polystyrene and plastic disposables by 2025, adopting fiber-based bowls. Several U.S. states and EU countries now ban foam foodware, accelerating kraft and bagasse adoption. You can find quality disposable paper bowls through multiple channels. Major retailers like Georgia-Pacific have expanded their compostable product lines. Online retailers and eco-conscious stores now stock these products. When evaluating suppliers, verify their claims carefully by requesting independent laboratory reports and certifications. Follow these steps to confirm product quality: PFAS-free and compostable claims require independent verification. A compostability certificate does not prove PFAS absence. Look for reputable suppliers who provide transparent documentation. Custom disposable paper bowls from trusted manufacturers meet both safety and performance standards. The availability of compostable paper bowls continues growing as more businesses recognize their value.   You have seen how the four comparisons settle the debate decisively. Environmental impact favors renewable materials like bagasse and bamboo. Recycling systems reduce virgin resource needs. Performance matches or exceeds plastic in heat resistance and durability. Compostability offers a clean end-of-life without centuries of persistence. Bulk purchasing closes the cost gap. Quick-service restaurants are leading the adoption of paper bowls, with many planning to phase out plastic disposables. This shift proves that quality and sustainability coexist. Make the switch for your next event or business. Choose trusted brands for reliable, certified compostable paper bowls. Small changes accumulate into meaningful environmental impact. Your choice today shapes a cleaner tomorrow.   FAQ Are compostable paper bowls safe for hot foods? Yes. Bagasse bowls withstand temperatures up to 220°F without warping or leaking. Bamboo bowls resist warping at 90°C for 60 minutes. Always check the certification label for microwave-safe claims before heating. These materials handle hot soups, curries, and saucy dishes effectively. What does "industrially compostable" mean? Industrial composting requires controlled conditions—high temperatures and humidity—that accelerate decomposition. Most compostable paper bowls break down within 60 to 90 days in these facilities. Your backyard bin rarely reaches those temperatures. Check the label for "industrially compostable" or "home compostable" to know what your setup can process. How do I verify a bowl is truly PFAS-free? Look for third-party certifications and laboratory reports. A compostability certificate does not prove PFAS absence. Request documentation showing targeted PFAS testing, not just Total Fluorine screening. Reputable suppliers provide transparent verification for their custom disposable paper bowls. Can I recycle paper bowls with food residue? No. Food contamination ruins recycling batches. Most paper bowls contain plastic or PLA linings that recycling facilities cannot separate. Composting offers the better end-of-life option. Scrape leftover food, rinse briefly, and send the bowl to an industrial compost facility instead. Do eco-friendly bowls cost significantly more? The gap narrows with bulk purchasing. Standard plastic bowls cost $0.05 to $0.10 per unit. Certified compostable paper bowls range from $0.20 to $0.50. Long-term savings from reduced disposal fees often offset the initial price difference.
  • Single Wall vs. Double Wall vs. Ripple Paper Coffee Cup: How to Choose the Right Paper Coffee Cup Single Wall vs. Double Wall vs. Ripple Paper Coffee Cup: How to Choose the Right Paper Coffee Cup Aug 18, 2026
    Picking the best paper coffee cup means balancing product costs with worker speed, storage space, cup strength, and customer safety. Single wall cups cost less to buy at first. Double wall designs keep drinks warm so customers stay comfortable. Ripple wall coffee cups offer the best heat protection and a solid grip during busy hours.   Cup Type 12 oz FOB Price Heat Insulation Sleeve Needed Grip Comfort Sturdiness Primary Application Single Wall $0.020–$0.030 Low Yes Basic Standard Iced or Sleeved Hot Drinks Double Wall $0.042–$0.062 High No Smooth High High-Volume Hot Espresso Ripple Wall $0.055–$0.075 Maximum No Textured Maximum Premium Delivery Takeaway   Key Takeaways Single wall cups cost less upfront but require extra sleeves for hot drinks. Double wall cups keep coffee warm up to 30 percent longer without sleeves. Ripple wall cups provide maximum heat protection and a safe, non-slip grip. Multi-layer cups eliminate sleeve steps to save staff up to 25 minutes per rush.   Single Wall vs. Double Wall vs. Ripple Paper Coffee Cup     Single Wall Cup Specifications and Layer Design Choose single wall options for simple drink operations. Manufacturers build standard single-wall paper coffee cup units using raw bleached kraft cupstock with a paper weight between 170 gsm and 280 gsm. Total PE-coated cupstock weight ranges from 190 gsm to 280 gsm. An inner plastic layer stops liquid leaks. Cold drink cups use a 15 to 18 micron lining. Hot drink cups need a 20 to 25 micron inside layer. Hot drinks at or above 60°C need a thicker 350 gsm paper base plus an extra paper sleeve to protect user hands from heat. Pick specific cup sizes based on different menu needs. A small 4 oz container holds 118 ml for single espresso shots or drink samples. Standard 8 oz and 12 oz choices hold 237 ml and 355 ml for hot cappuccinos and lattes. Bigger 16 oz, 20 oz, and 24 oz sizes hold 473 ml, 591 ml, and 710 ml for cold drinks or frappes.     Double Wall and Ripple Wall Engineering Get better heat control when you switch to multi-layer paper coffee cup designs. Factories make double wall paper coffee cups by attaching a second paper outer wall over an inside liner. This two-layer build creates a trapped 3 to 5 mm space. Trapped air offers a low heat flow rate of 0.024 to 0.026 W/mK compared to normal paper at 0.05 W/mK. This air space cuts heat transfer and keeps hot drinks warm up to 30% longer. Select ripple cups for a strong hand grip and great heat protection. Factories glue a wavy paper layer onto the outer wall surface. This bumpy outer layer creates many tiny air pockets that shield customer hands from high heat. The wavy shape lets your customers hold drinks over 80°C safely without needing extra sleeves.      Insulation Performance and Safety Comparison   Good heat control helps you serve hot drinks safely. Double wall paper coffee cups keep drinks 35% warmer than sleeved single wall cups over an hour. This strong insulation removes your need to buy extra cardboard sleeves. The smart two-layer build holds in heat very well. In 60 minutes, a single wall cup with a sleeve loses 26°C or 31% of its starting heat. By contrast, a double wall paper cup loses just 19°C or 22% of its warmth in that same time. Your coffee shop customers can enjoy hotter coffee much longer on their morning drive. Double wall retains heat 35% better than single wall + sleeve over 60 minutes. The ASTM C1055 test rule checks outer surface safety for hot drink cups. Testers pour 185°F liquid into cups and check outer temperatures after two minutes. For safe and easy holding, the outside of the cup must stay at or below 115°F.   Cup Construction Exterior Temperature After 2 Min Hold Comfort Relative to 115°F Limit Single-wall, no sleeve 155–165°F Exceeds limit; comfortable only 0–8 s; requires sleeve or double-cupping Single-wall with sleeve 115–125°F At the limit; comfortable 15–30 s; acceptable for short holds Ripple-wall 115–130°F Slightly above limit; comfortable 60–90 s; good for moderate use Double-wall 100–112°F Below limit; comfortable indefinitely   Bare single wall cups reach 155–165°F right after you fill them. People can hold these plain cups comfortably for only 0 to 8 seconds. Adding a sleeve to a single wall cup lowers temperatures to 115–125°F for 15 to 30 seconds of easy holding. Wavy ripple cups hold heat 30% to 40% better than plain single wall options. Their bumpy outer layer stays 15°C to 20°C cooler to protect hands from painful burns. People can hold ripple cups comfortably for 60 to 90 seconds. Double wall cups stay between 100°F and 112°F on the outside. This temperature stays safely below the 115°F limit, so buyers can hold drinks as long as they like.   Structural Integrity and Sturdiness Under Heat Hot liquids weaken thin paper cups during long takeaway trips. High heat softens raw paper fibers and melts inner protective plastic coatings. Regular single wall cups bend easily under a firm grip when filled with hot espresso. Your cafe staff must use two cups or add cardboard sleeves to stop cups from caving in during rush hours. These extra steps cause slow customer service lines. Multi-layer paper designs fix these weak cup problems easily. Double wall coffee cups use two layers of thick paperboard. This strong build stops the side walls from crushing when customers squeeze their cups tightly. Bumpy ripple cups add stiff vertical ridges to the outside paper layer. These textured outer ridges give you a better grip and protect against side bumps on the go. You can find strong double wall paper cup items at elementscup. Buying sturdy cups stops messy spills, keeps customers happy, and speeds up busy shop service.   Total Cost of Ownership and Efficiency Calculate all product costs carefully before buying supplies for your cafe shop. Many coffee business owners look only at the basic unit price. You need to calculate the full total to discover your real cost per drink: total cost = single wall unit price + sleeve price + storage cost + labor time per order.   Single Wall Sleeve Expenses vs. Multi-Layer Unit Cost Check the base prices for standard drink containers first. A single wall paper coffee cup costs from $0.020 to $0.030 per item. This starting price seems cheap at first glance. Hot drinks like lattes require protective sleeves to keep customer hands safe. Purchasing extra cardboard sleeves adds another $0.015 to $0.025 to every order. Storage overhead adds extra hidden costs to your monthly business budget. Storing separate boxes of sleeves takes up useful shelf space in your supply room. Small storage areas stay open for key coffee beans and ingredients when you drop sleeve boxes. You have to track two vendors or place double orders. Shipping fees also go up when ordering multiple small shipments. Multi-layer items streamline your purchasing pipeline into one clear item line: Packaging Selection Base FOB Unit Cost Sleeve Add-On Cost True Total Unit Cost Range Storage Footprint Impact Single Wall Option $0.020–$0.030 $0.015–$0.025 $0.035–$0.055 High (Requires double box space) Double Wall Option $0.042–$0.062 $0.000 $0.042–$0.062 Compact (Single box unit inventory) Ripple Wall Option $0.055–$0.075 $0.000 $0.055–$0.075 Compact (Single box unit inventory)   Buying double wall paper coffee cups costs between $0.042 and $0.062 each. Top ripple cups cost from $0.055 to $0.075 each. Basic price checks show that single wall cups with sleeves cost about the same as built-in double wall paper cup items. These savings balance out early stock costs fast. Picking built-in designs removes extra supply tasks entirely.   Rush-Hour Service Speed and Labor Impact Work steps during busy morning rushes directly shape your overall daily sales. Single wall setups make your workers perform extra physical steps for each hot drink order. A worker grabs a cup, fills hot coffee, takes a cardboard sleeve, slides it on, and caps the drink. Some cafes use two cups instead, which wastes two plain cups on one drink. Integrated multi-layer cups optimize your service workflow during peak hours: A worker grabs a ready double wall coffee cup right from the storage stack. A worker pours hot coffee into the sturdy cup without burning any hands. A worker pushes the tight lid onto the top rim in one smooth motion. A worker hands the finished drink right to the waiting coffee customer. This simple work method saves your team 3 to 5 seconds on every drink. Making 300 hot drinks during a morning rush saves up to 25 full work minutes. This saved labor time cuts your wage costs for every cup served during busy shifts. Faster service lines let your shop fill more customer orders every hour. Quick service lowers customer waiting times, boosts total morning profits, and keeps your staff from getting tired.   Storage Footprint and Branding Surface   Stackability Density and Inventory Footprint Storage space directly impacts daily coffee shop management. Single wall paper cups stack tightly inside shipping boxes. Their thin side walls allow easy storage on inventory shelves. You can place many single wall units inside small stockroom areas. This compact stacking saves useful shelf space for extra coffee beans, syrup bottles, and paper napkins. Multi-layer paper cups need larger storage areas inside your shop stockroom. Double wall coffee cups use an air gap that makes outer rims wider. Ripple cups add a thick textured layer around outer paper walls. These extra layers lower total nesting depth inside shipping boxes. So, one master box holds fewer multi-layer units than single wall options. You need extra shelf space when stocking double wall paper cup.   Print Surface Quality and Branding Suitability Your paper drink container serves as a mobile billboard on city streets. Single wall designs and double wall paper coffee cups feature smooth paper outer surfaces. Printing machines add bright colors, fine text lines, and detailed brand logos onto these flat surfaces. Smooth double wall paper cup choices show custom graphics with great visual clarity. You can print sharp artwork and exact color tones to build high brand recognition with local customers. Ripple cups offer a unique look and feel for your takeaway menu. Bumpy outer waves form a strong textured surface around the container. Fine text lines and complex multi-color artwork can bend across these raised vertical ridges. Standard printing works best with bold logos and simple shapes on textured paper walls. Yet, the firm grip of ripple cups gives a memorable hand feel that shows your commitment to quality coffee service.   Strategic Selection Matrix for Operators   High-Volume Takeaway vs. Specialty Espresso Bars Busy takeaway shops need quick workflows and low costs. You can improve supply plans by picking 12 oz options as main stock. The 12 oz cups make up 35-40% of orders in busy chains. Paper cups should form 60-70% of total packaging stock. Matching inventory with customer demand lowers buying costs by 12-18%. Busy shops stop service delays during peak hours when workers use simple standard cup sizes. Specialty cafes focus on drink warmth and customer comfort. Double-wall cups put an air gap between two paper layers to trap heat inside. The firm outer wall stays cool so cups do not collapse easily. Ripple-wall cups use a bumpy texture that forms a natural air layer for heat protection. This raised shape gives customers a firm grip and keeps hands safe without needing extra paper sleeves.   Choosing the Right Paper Coffee Cup for Your Business Order details help you plan stock needs for different paper cup styles. Plain white 7 oz single wall cups need a 10,000-piece min order and take 3–5 workdays. Custom printed 12 oz single wall units require 30,000 pieces and take 7–10 workdays. Insulated 16 oz double wall cups take 7–9 workdays for 20,000 pieces. Bumpy 24 oz ripple wall designs need 15,000 pieces and take 6–8 workdays. Flexible buying choices can reduce your initial product costs. Helpful suppliers allow small custom runs starting at 5,000 pieces for simple single-color prints. Eco-friendly PLA double-wall items need a 20% higher min order than basic PE choices. Ordering paper coffee cups together with matching lids and straws reduces overall order limits by 25%. Always check stock room space, as compostable cups last only 8 months on the shelf. Single wall cups drop your early prices on cold or sleeved drinks. Double wall and ripple wall options protect hands, trap heat, and stop side walls from crushing. Use this simple four-step purchasing list to pick the best paper coffee cup for your business: Check your total sales numbers for hot and cold drinks. Check your total storage room and box space limits. Test warm cup samples at 90°C for lid tightness and leaks. Add up all unit prices including shipping, insurance, and taxes. Get sample boxes to check real cup quality before you place big custom orders.   FAQ   Do double wall paper coffee cups eliminate the need for sleeves? Yes. Double wall paper coffee cups trap a 3 to 5 mm air layer between two paperboards. This design keeps outer temperatures from 100°F to 112°F. Your customers can hold hot drinks comfortably without buying or adding extra cardboard sleeves. How do ripple cups protect hands from hot liquids? Ripple cups feature a wavy, textured paper layer glued onto the outer wall. These vertical ridges make air pockets that keep the outer surface 15°C to 20°C cooler than plain single wall choices. You give customers a safe, non-slip grip on hot takeaway drinks. How much time do double wall coffee cups save during peak hours? Ready-to-use double wall coffee cups save your staff 3 to 5 seconds per hot drink order. Workers skip the extra step of sliding on cardboard sleeves during morning rushes. Serving 300 hot drinks saves up to 25 full work minutes every day. Where can you buy sturdy double wall paper cup options? You can explore high-quality double wall paper cup inventory at www.elementscup.com. Their multi-layer paper containers give great heat retention, stop side-wall crushing under pressure, and help speed up customer service during your busiest operational hours.  
  • How Custom Paper Cups Help Coffee Brands Build Stronger Customer Recognition How Custom Paper Cups Help Coffee Brands Build Stronger Customer Recognition Aug 12, 2026
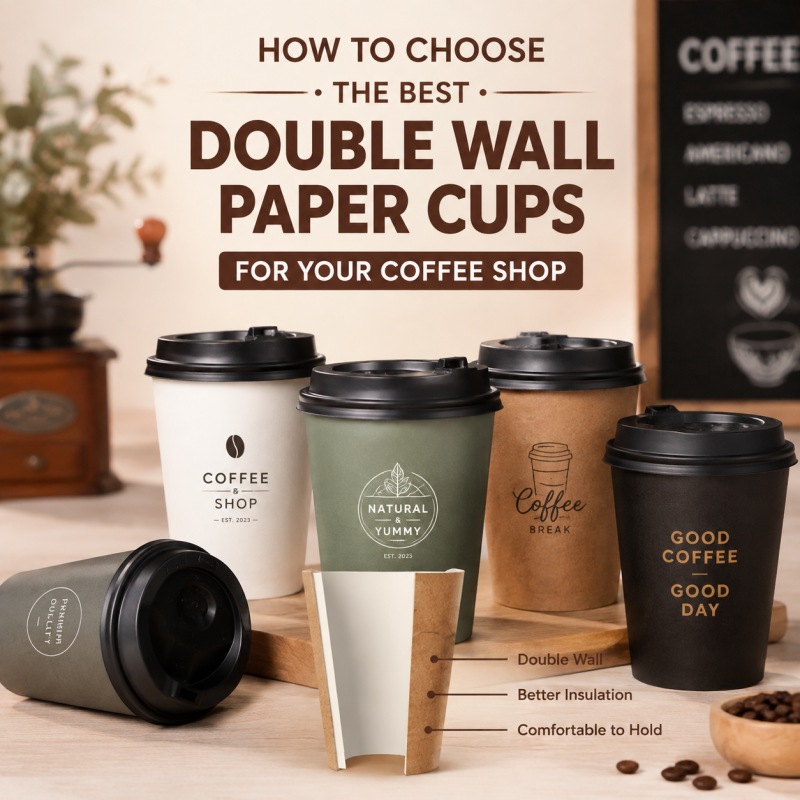
    You turn every daily beverage transaction into passive local advertising with custom paper cups. Generic packaging fails to capture valuable equity. Plain containers waste dynamic real-world touchpoints every single morning. In contrast, custom artwork creates an immediate visual anchor in outdoor spaces. Passersby instantly notice each coffee buyer walking through busy streets. This constant physical exposure powers your entire local marketing engine efficiently. You transform routine coffee consumption into stronger brand recognition and immediate social proof. This persistent visual presence steadily elevates customer recognition across the neighborhood. Ultimately, your strong brand identity drives deeper long-term retention among daily coffee drinkers in your community.   Key Takeaways Custom paper cups turn daily takeout drinks into active mobile advertisements on busy neighborhood streets. Branded packaging offers a cheaper way to reach local customers compared to digital ads. Eco-friendly materials and thoughtful cup designs build immediate customer trust and show quality. Interactive QR codes on paper cups easily connect daily physical orders to digital loyalty rewards.   How Custom Paper Cups Act as Mobile Billboards     Maximizing Brand Visibility on the Street Every morning, local customers walk out of your cafe carrying fresh beverages. These active pedestrians carry your distinctive logo across crowded city sidewalks, bustling train stations, and corporate office halls. Heavy foot traffic continually converts everyday carryouts into passive street-level advertising for neighborhood cafes. Each portable cup transforms an ordinary customer into an active walking ambassador for your business. Prospective buyers notice your logo repeatedly during their daily morning commutes. This persistent high-frequency exposure creates familiar visual anchors in busy public spaces. People naturally remember your shop location whenever they crave gourmet coffee later in the afternoon. Cost-effective physical marketing tools generate maximum brand visibility without expensive ad budgets. You can reach hundreds of local residents every day simply by serving drinks in branded packaging. Compare the average cost per thousand impressions (CPM) of common advertising channels in the table below: Advertising Medium Cost Per Thousand Impressions (CPM) Branded Paper Cups $3 Instagram Ads $8 - $15 Google Ads (Display Network) $12 - $25 Billboard $5 - $10   Turning Takeout Orders Into Daily Touchpoints Every takeaway order provides a valuable free brand impression right in the hands of active consumers. High-quality physical packaging keeps hot and cold drinks secure while continually boosting local visibility throughout the community. Elements Paper Cups offers sturdy single-wall designs for iced coffee, juice, and cold beverages. For hot cocoa or specialty tea, durable double-wall construction eliminates the need for extra paper sleeves entirely. Properly insulated containers allow patrons to hold hot beverages comfortably while walking long distances across town. Your custom printed graphics stay completely visible without annoying cover-ups during daily drink consumption. Repeated exposure to branded coffee cups builds long-term recall and deep customer trust. According to research from the Advertising Specialty Institute, 85% of people remember the advertiser on a promotional product after seeing it repeatedly. Promotional drinkware generates an average of 1,300 impressions throughout its lifetime, costing about 1 cent per impression. Furthermore, 80% of customers say they have a better impression of a brand after receiving personalized cups or promotional merchandise. This repeated exposure fosters positive associations during ordinary daily routines, which directly supports customer retention over time. Real-world commercial results demonstrate the financial power of customized packaging solutions: A small coffee shop introduced custom cups featuring a distinctive color scheme, playful logo, and catchy tagline. Customers began posting photos on social media platforms, tagging the shop and boosting its digital presence. Within six months, the shop saw a 20% increase in foot traffic, attributed to social media engagement and word-of-mouth. Thoughtful packaging design elevates your everyday customer experience significantly. Strategic visual presentation increases brand exposure across your target neighborhood every single morning. Elements Packaging helps you maintain complete visual consistency and strong brand loyalty across both cold and hot menus. Ultimately, you turn routine daily coffee orders into dynamic marketing assets when you serve drinks in custom paper cups.   Elevating Customer Recognition Through Design   Strengthening Brand Quality and Perception Visual elements directly influence how consumers evaluate your menu offerings. Vibrant color palettes and bold logos on custom paper cups communicate professional value immediately. You signal exceptional craftsmanship when you select high-contrast colors and strategic graphic placements. Industry research proves container colors alter taste perceptions directly. For instance, testing shows 80% of females reported a richer aroma from red containers, while 73% found coffee in brown containers too strong. Precise visual choices shape expected flavor before a customer takes one sip. Gourmet coffee lovers appreciate thoughtful visual details on their morning containers. Color psychology plays an essential role in customer attraction. A professional cup design uses premium print finishes to create lasting tactile cues. Smooth satin coatings feel refined to the touch. In contrast, textured surfaces convey physical strength. Strong contrast between glossy graphics and matte backgrounds demonstrates careful attention to detail. Embossed patterns offer tactile depth that engages customer senses directly. This physical interaction transforms ordinary takeaway drinkware into a memorable physical touchpoint. Lab studies from the U.S. Postal Service Office of Inspector General and Temple University found that physical ads create stronger memories and higher perceived value than digital alone. You elevate overall cup quality by combining sharp visual cues with superior physical stability. Reliable structural integrity prevents unexpected spills during transport. Customers associate this physical dependability with high product standards. High-grade physical packaging protects drink temperatures while maintaining surface comfort for walking consumers. Distinctive physical features shape consumer perception effectively: Visual Identity: Consistent colors and logos build a mental link between your beverage and your brand. Tactile Cues: Sturdy double walls and leak-proof lids show respect for your product. Quality Signals: Unique designs transform every takeaway drink into a premium experience. Recommendation Triggers: Passersby notice attractive packaging in public spaces and try new cafes based on visual appeal. Every well-crafted container serves as a proxy recommendation. Thoughtful design choices drive stronger word-of-mouth marketing across your neighborhood.   Utilizing Eco-Friendly Packaging to Build Trust Packaging materials act as silent communicators of your corporate values. Modern consumers frequently interpret sustainable material choices as clear signals of ethical commitment. Eco-friendly packaging choices reflect positively on your entire corporate philosophy. You demonstrate genuine environmental responsibility by choosing branded coffee cups built from renewable resources. Elements Packaging provides eco-conscious solutions engineered with FSC-certified paper pulp. These reliable options eliminate reliance on standard unsustainable materials while preserving complete beverage integrity. Innovative material options allow you to protect local ecosystems without sacrificing daily operational convenience. You can select custom-printed coffee cups featuring plant-based PLA coatings designed for industrial compostability. Alternatively, you can choose advanced plastic-free aqueous barrier coatings for seamless recycling. These sustainable alternatives reduce your overall environmental footprint while providing reliable leak-resistant performance. Every sustainable cup serves a functional purpose while reducing environmental impact significantly. Selecting sustainable materials creates distinct custom artwork that appeals to eco-conscious patrons. Transparent eco-friendly choices strengthen emotional connections with environmentally conscious consumers. Buyers feel genuine satisfaction when supporting businesses that protect natural resources actively. This positive alignment transforms an ordinary daily transaction into a meaningful brand interaction. Furthermore, offering responsible custom packaging deepens customer loyalty over time. Distinctive sustainable branding builds lasting trust, boosts local brand recognition, and elevates every customer experience.   Leveraging Custom Drink Cups for Digital Engagement   Driving Social Media Shares With Unique Artwork You can transform everyday physical containers into viral social media assets. In 2014, Starbucks launched the #WhiteCupContest on Twitter and Instagram. Customers doodled on white coffee cups and shared their creative drawings online. This effort generated over 4,000 entries and millions of impressions within three weeks. This initiative directly supported a period of record sales for the enterprise. You build massive digital engagement when you invite active patrons to decorate physical packaging. Distinctive cup designs tap directly into user social currency. Customers love sharing pictures of custom drink cups across personal online networks. Low participation barriers encourage regular patrons to post photos during ordinary morning routines. In 2016, the #RedCupArt challenge repeated this successful framework on iconic holiday cups. Unique visual artwork instantly boosts local visibility and elevates direct marketing campaigns. Integrating Interactive QR Codes for Loyalty Dynamic technology connects physical custom drink cups directly to digital brand interactions. You can print unique custom graphics on sturdy custom paper cups to attract tech-savvy shoppers. Coffee shops can place scannable codes on cups, packaging, or receipts. Each scan could reward customers with loyalty points for future discounts. This efficient strategy lowers printing expenses while building strong customer loyalty across your target neighborhood. Digital incentives turn ordinary beverage carryouts into active repeat visits. You strengthen direct relationships without spending extra money on printed physical paper coupons. Real shop data demonstrates the clear marketing value of smart packaging placements. The Daily Grind Coffee Shop printed scannable codes on cup sleeves with a "Scan for a free pastry" promotion. Analytics showed QR codes on coffee cup sleeves achieved the highest scan rates among all tested promotional placements. You turn branded drinkware into an interactive asset by placing scannable elements next to official logos. Elements Packaging helps cafes build lasting digital engagement through versatile drinkware options.   Creating a Unified Brand Packaging Ecosystem   Aligning Cup Styles Across Hot and Cold Menus You create a cohesive physical presentation when you match your packaging options across your entire menu. You should serve espresso in small containers while reserving larger vessels for milk-based lattes and iced tea. Standardizing your daily portion sizes builds immediate confidence among morning patrons. Elements Packaging helps you maintain this visual harmony across all beverage temperatures effortlessly. Matching your packaging style to specific menu items transforms daily orders into a unified brand presentation. Proper container alignment ensures every patron receives an attractive drink while walking through public spaces. Uniform visual details build familiarity across your entire product line. You reinforce quality standards when cold beverages and hot drinks share identical colors, logo placements, and typography. Companies with consistent packaging experience 23% higher customer retention rates. Customers instantly recognize your products in any environment. Standardized visual design elements build strong visual recall over time across your local community. This visual harmony reassures buyers and simplifies their purchasing choices every morning.   Reinforcing Identity Across Every Touchpoint A seamless packaging ecosystem extends your market reach beyond the service counter. Using custom paper cups creates a physical touchpoint that shapes customer perceptions directly. High-quality presentation reinforces professional service across all store locations consistently. Marketers report compelling financial benefits from maintaining uniform visuals across all channels: Metric Financial and Loyalty Impact Visual Identity Trust 73% of consumers trust companies with a consistent visual identity. Revenue Attribution 68% of marketers report consistent branding increased revenue by at least 10%. “The most common mistake is inconsistency across visual elements, using different logos, colors, or messaging across various platforms.” — Joshua Schmitt, Senior Graphic Designer Every takeaway order strengthens your presence across the neighborhood. Using branded coffee cups reinforces your identity during daily routines. Furthermore, serving delicious coffee in branded drinkware turns everyday coffee consumption into a memorable customer experience. This thoughtful attention to detail encourages repeat visits while elevating overall customer satisfaction.   Custom paper cups provide powerful marketing advantages for every modern business. You turn a simple operational expense into a high-return local marketing tool. Daily drink carryouts generate persistent visual exposure across busy neighborhood streets. Now you can upgrade your coffee shop packaging strategy through three straightforward steps: Select signature design elements that highlight your unique brand identity clearly. Choose appropriate vessel sizes like 8oz, 12oz, and 16oz to fit your entire drink menu. Align your physical packaging with digital loyalty programs to reward repeat buyers continuously. Serving delicious coffee in branded coffee cups secures maximum long-term customer recall across your entire target community.   FAQ What sizes do custom paper cups come in? Elements Packaging offers custom paper cups in popular commercial sizes. You can choose 8oz, 12oz, 16oz, and 22oz options for your beverage menu. These standard sizes accommodate everything from espresso shots to large iced coffees.   How do branded paper cups improve local marketing? Branded paper cups turn everyday takeout orders into mobile advertisements across your neighborhood. Walking customers display your unique logo to nearby pedestrians. This continuous visual exposure builds immediate brand recognition and drives new patrons to your shop.   Are eco-friendly packaging options available for custom drinkware? Yes. Elements Packaging manufactures sustainable options using FSC-certified paper pulp. You can select industrial-compostable PLA coatings or plastic-free aqueous barrier coatings. These eco-friendly materials deliver reliable leak-proof performance while protecting the environment.   Should you choose single-wall or double-wall paper cups? Single-wall cups work best for iced coffee, juice, and cold drinks. Double-wall cups feature extra insulation to keep hot beverages warm. This durable double-wall construction keeps customer hands comfortable while eliminating the need for extra paper sleeves.  
  • How to Choose the Best Double Wall Paper Cups for Your Coffee Shop How to Choose the Best Double Wall Paper Cups for Your Coffee Shop Aug 06, 2026
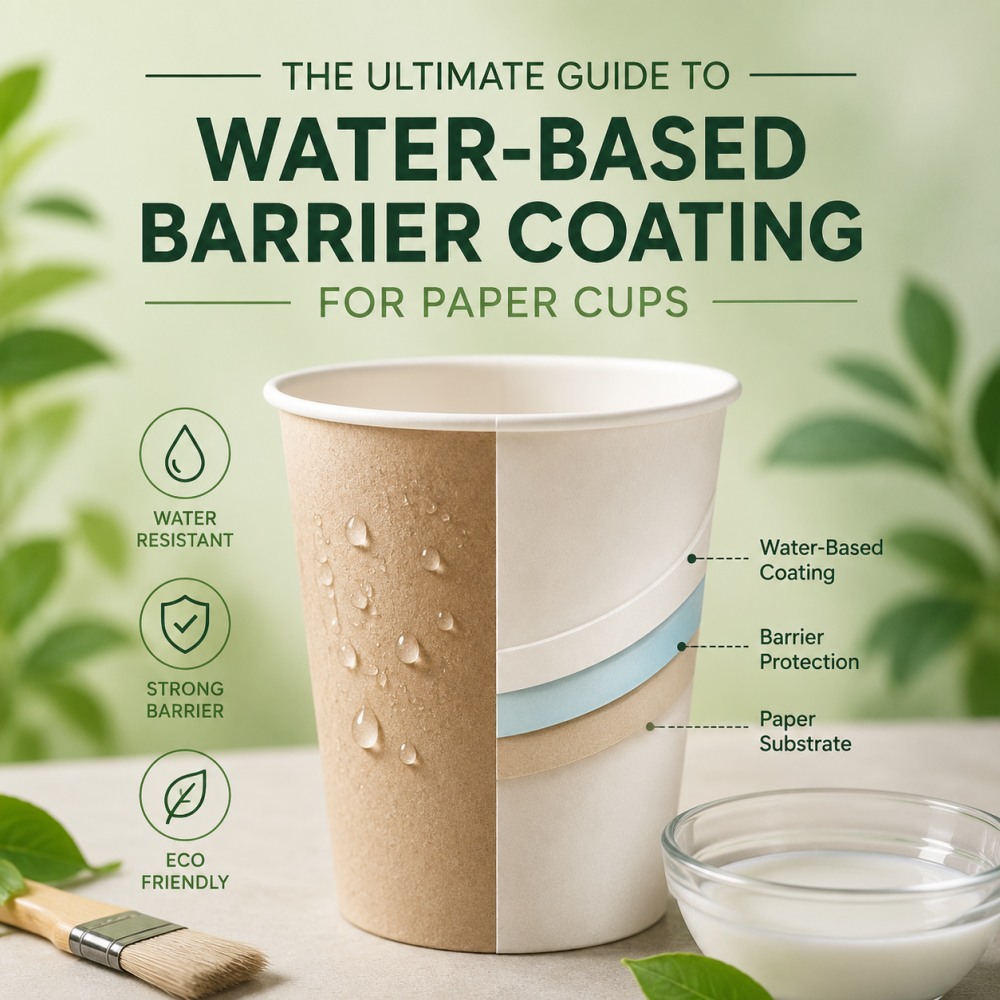
    As a coffee shop owner, your drinkware directly shapes customer satisfaction, brand perception, and daily operational safety. Hot coffee demands containers that protect hands while keeping beverages warm. Choosing high-quality double wall paper cups requires careful evaluation of five essential factors: heat insulation performance, structural durability, lid fitment, custom branding capability, and unit cost. Evaluating physical cup construction prevents costly cafe accidents. Weak sidewalls collapse easily under pressure, and ill-fitting lids cause messy spills. Furthermore, poor insulation forces customers to use extra sleeves, driving up expenses. Inspecting paper firmness, seam tightness, and rim consistency ensures your takeaway cups deliver a safe, premium experience.   Key Takeaways Double wall paper cups keep drinks hot longer and protect customer hands without extra sleeves. High-density paperboard and tight rims prevent messy leaks, cup collapses, and burn accidents. Standardized top rim sizes save valuable storage space and speed up busy coffee service. Custom printed eco-friendly cups improve your brand image and protect the environment.   Evaluate Insulation and Material Quality Advantages of Double Wall Paper Cups You improve daily cafe operations when you select double wall paper cups for your hot beverage menu. The outer paper layer creates an insulating air gap that slows heat loss. This clever physical structure protects your customers' hands from high beverage temperatures. You eliminate the need for separate cardboard sleeves entirely. Removing extra sleeves saves valuable back-of-house storage space. Eliminating sleeves also cuts down drink preparation time during morning rush hours. Proper heat insulation ensures a premium drinking experience for every customer. Superior heat retention maintains your specialty coffee at optimal serving temperatures longer. Extended Thermal Duration: Double-wall paper cups maintain drink temperatures effectively for 20 to over 30 minutes, whereas single-wall alternatives lose heat much faster, lasting only about 10 to 15 minutes. Insulation Mechanism: The structural design incorporates an intentional air gap between two layers of paper, which functions as an insulating barrier that minimizes heat conduction. Metric / Thermal Property Performance Gain of Double-Wall vs. Single-Wall Key Observation / Test Detail Overall Insulation Improvement ~60% better Measured when filled with 95°C hot water Outer Wall Surface Temperature 33%–40% reduction (24°C–27°C lower) Maintains surface near 50°C instead of >80°C Effective Thermal Conductivity 44% lower Trapped 3–5mm air layer approaches air's thermal conductivity Heat Transfer / Temp Rise Rate Reduced to 41.7% of single-wall rate Significantly slows down heat loss over time Using double wall paper cups protects customer comfort while maintaining beverage taste over time. Your customers enjoy hot drinks safely without burning their fingers.   Paper Density and Wall Structure Paperboard density directly dictates physical cup strength and thermal retention. Packaging manufacturers measure paper weight in grams per square meter (GSM). High paperboard GSM prevents sidewall softening when hot liquid fills the container. Choosing a robust disposable double-walled coffee cup keeps structural integrity intact throughout long customer commutes. You must select appropriate thickness ranges for both interior and exterior walls to guarantee maximum product durability in daily cafe operations. High density paperboard provides rigid wall support during daily customer handling. Layer Recommended GSM Range Inner Wall 180 – 250 GSM Outer Wall 200 – 300 GSM Combining these heavy paperboard layers creates a sturdy rigid frame. Higher density paperboard effectively resists internal moisture absorption over time. Proper thickness keeps cup sidewalls firm during firm squeezing. Firm sidewalls protect your customers from accidental cup collapsing or liquid spills. You maintain consistent drink presentation across every service shift by ordering correct material densities. Durable cup walls prevent hot liquids from leaking through weakened paper seams.   Rim Rigidity and Leak Prevention A tightly rolled rim provides essential structural support to the upper cup edge. Firm rim rigidity prevents cup collapsing when customers apply downward pressure to attach drink lids. You safeguard your business against messy spill accidents by verifying rim tightness during sample evaluations. Precise rim circularity ensures an airtight lid seal for busy on-the-go patrons. Uniform rim dimensions stop liquid seepage along side seams during transport. Premium double wall paper cups maintain shape under heavy use, ensuring safe transport for every hot beverage you serve. Strong rims retain structural integrity under continuous handling. You build customer trust when your drink packaging prevents accidental burn injuries and clothing stains. Quality testing guarantees reliable lid fitment across high-volume daily beverage sales.   Select Sizes and Compatible Lids Matching Capacities to Menu Items Selecting correct cup capacities protects original beverage flavor profiles and increases overall customer satisfaction. In North America, offering 4 oz, 8 oz, 12 oz, and 16 oz options covers about 95% of typical menu orders. Core drivers like 12 oz and 16 oz sizes represent 65%–75% of total daily cup volume. Continental European specialty menus rely on a standard 200–300 ml range for takeaway orders, with ~400 ml acting as maximum menu capacity. Matching physical cup volumes preserves intended coffee recipes. An 8oz double wall paper cups design holds cappuccinos within 150–200ml total volume, maintaining rich espresso taste without milk dilution. A 12oz cup holds double espresso shots alongside 250–270ml of steamed milk with proper headroom. Furthermore, a 16oz size accommodates large lattes and cold ice displacement effortlessly.   Securing Leak-Proof Lid Fits Precise lid fitment prevents hazardous drink spills and protects customer safety during busy morning commutes. You must evaluate physical snap-fit lid security against the top rolled rim profile of your chosen double wall paper cups. Strong rim engagement keeps lids anchored tightly when customers apply firm handling pressure. Proper lid closure maintains internal beverage temperature effectively and stops liquid seepage along side paper seams. Weak lid fitment causes dangerous liquid drips during active customer movement. Verifying tight lid seals across daily sample batches protects customer clothing and maintains high service standards.   Standardizing Rim Diameters Standardizing top rim diameters improves daily operational efficiency across your entire beverage menu. Utilizing standardized rim sizes reduces your required cup storage footprint by an estimated 15–20%. Baristas grab universal lid designs quickly during rush periods without searching through matching size variants. Eliminating redundant lid SKUs lowers overall working capital tied up in unused storage inventory. Streamlining rim profiles minimizes drink preparation mistakes during peak operational sales shifts. Equipping your business with a uniform disposable double-walled coffee cup setup speeds up order fulfillment consistently.   Choose Sustainable Double Wall Paper Cups Eco-Friendly Lining Options You must select correct eco-friendly lining materials to reduce environmental impact. Modern cafes prefer sustainable barrier coatings on double wall paper cups over traditional plastic linings. Feature PLA Coating Aqueous Coating Environmental Breakdown Requires industrial composting streams; degrades within 3–6 months. Plastic-free; home or soil compostable; easily recyclable. Thermal Performance Tends to soften above 80°C. Offers high heat resistance. Official certifications verify eco-friendly claims for your shop. Look for BPI certification following ASTM D6868 or ASTM D6400 standards in North America. European markets recognize TÜV Austria testing standards like OK Compost INDUSTRIAL and OK Compost HOME under EN 13432. These certifications guarantee full biodegradation within commercial composting facilities.   Custom Branding with Elements You convert standard drinkware into powerful promotional assets using Elements packaging solutions. Strategic visual design strengthens business identity across every service shift. Converting everyday takeaway items into mobile billboards shifts packaging from a standard operational expense into a strategic marketing investment that enhances brand recognition and fosters long-term customer loyalty. Custom logo printing builds strong brand recall during morning rushes. Customers carrying a customized disposable double-walled coffee cup act as walking advertisements across offices and public transit. Aesthetic packaging also inspires patrons to post photos on social media channels, generating organic marketing reach.   Print Quality and Surface Finishes Selecting advanced printing methods ensures crisp graphics on smooth outer cup walls. Offset Printing: Delivers sharp graphics alongside high color fidelity using precise Pantone color matching. Embossing & Foil Stamping: Provides a tactile finish that adds an elegant look to custom packaging. Food-safe soy and water-based inks deliver vibrant imagery while maintaining strict safety standards. These specialized inks offer thermal stability and appropriate viscosity, so pigments never degrade during hot beverage sales. Strong ink adhesion prevents smudging on customer hands, keeping your printed branding clear and professional.   Analyze Total Cost and Supplier Logistics Calculating True Unit Cost You evaluate total packaging expenditure by looking beyond the base purchase price. Investing in double wall paper cups eliminates the extra cost of separate cardboard sleeves entirely. You calculate actual item expenses using a plain formula: total unit cost = combined cup and freight expense / total volume. Sourcing requirements depend directly on your custom branding goals. Plain stock cups require baseline order volumes between 1,000 and 5,000 units. Basic custom logo prints raise minimum orders to 10,000 units. Complex full-color designs demand larger runs between 30,000 and 50,000 units due to factory printing constraints.   Managing Order Quantities and Storage Safe warehouse protocols preserve the structural strength of every disposable double-walled coffee cup shipment. You store inventory within a temperature range of +5°C to +25°C while maintaining ambient relative humidity near 55%. Humidity levels above 60% cause mold growth, while levels under 40% make paper brittle. You allow new stock to adjust inside sealed packaging for 2 to 4 days before opening. Proper stacking prevents carton damage during seasonal climate shifts. You maintain a clearance distance of at least 45 cm between product stacks and exterior walls to promote air circulation.   Choosing Reliable Supply Partners Partnering with dependable supply vendors like Elements protects your daily cafe operations from inventory shortages. You demand high performance standards, including a minimum 95% on-time delivery rate. Written service level agreements guarantee consistent restocking schedules for your business. Strict quality control protocols keep defective products off your service counter. You verify that your supplier maintains an acceptable quality level with an AQL under 0.4% defect threshold. Physical sample testing across separate production runs confirms rim tightness and wall strength before you sign long-term supply contracts.   Selecting ideal double wall paper cups requires careful evaluation of key performance factors: Superior thermal insulation maintains safe outer temperatures using an integrated air gap. Smooth interior linings prevent sogginess, while high paperboard density maintains structural rigidity. Precise rim dimensions prevent leaks, and FSC-certified paper supports environmental sustainability. Non-smudge custom printing using food-safe inks enhances brand visibility on takeaway orders. Audit your current drinkware inventory today. You should request sample kits from Elements to evaluate physical cup quality, heat retention, and lid security directly. Contact Elements now to place an order that aligns with your daily operational needs and budget goals.   FAQ Why should you choose double wall paper cups over single wall cups with sleeves? Double wall paper cups feature an integrated air gap that improves thermal insulation by about 60%. This design eliminates separate cardboard sleeves entirely, saving valuable back-of-house storage space and speeding up drink preparation during peak morning rush hours while keeping customer hands comfortable. What minimum order quantities should you expect for a customized disposable double-walled coffee cup? Order minimums depend directly on your design requirements. Plain stock cups require baseline orders between 1,000 and 5,000 units. Basic custom logo prints raise minimum order quantities to 10,000 units, while full-color custom artwork requires larger runs between 30,000 and 50,000 units. How long do double wall paper cups keep hot beverages warm? Quality double wall paper cups maintain serving temperatures effectively for 20 to over 30 minutes. The trapped air layer lowers effective thermal conductivity by 44%, slowing drink heat loss significantly compared to single-wall alternatives that lose warmth within 10 to 15 minutes. How do you verify eco-friendly claims for your disposable double-walled coffee cup inventory? You verify sustainability claims by checking product certifications directly. Look for BPI certification following ASTM D6868 or ASTM D6400 standards in North America. For European distribution, confirm TÜV Austria ratings such as OK Compost INDUSTRIAL under EN 13432 to ensure full commercial breakdown.
  • The Ultimate Guide to Water-Based Barrier Coating for Paper Cups The Ultimate Guide to Water-Based Barrier Coating for Paper Cups Jul 29, 2026
    You see water based coating paper cup solutions gaining attention because they use innovative, plastic-free technology. This approach supports the move from plastic to paper food packaging. Water-based coatings help you meet strict environmental standards. Recent regulations push for eco-friendly materials. Regulation Impact on Water-Based Coatings SUPD Promotes compliance with recycling standards, encouraging environmentally friendly materials. PPWR Drives the shift towards materials that align with circular economy principles, reducing compliance risks. You can choose options that comply with SUPD and PPWR, using bio-based materials for a sustainable future.     Key Takeaways Water-based coatings provide a plastic-free solution for paper cups, aligning with environmental regulations and reducing plastic waste. These coatings enhance recyclability, allowing cups to be processed with regular paper, which helps minimize landfill waste. Water-based coatings improve food safety by avoiding harmful chemicals and reducing the risk of microplastics in beverages. Choosing water-based coatings supports a positive brand image, appealing to consumers who prioritize eco-friendly products. Investing in water-based coating technology can lead your business towards sustainability while maintaining product performance.   What Is Water Based Coating Paper Cup? How Water-Based Barrier Coating Works You may wonder how a water based coating paper cup achieves its protective qualities without plastic. The answer lies in the dispersion technique. Manufacturers apply a liquid water-based dispersion directly onto the paperboard. This layer dries to form a thin, flexible barrier that keeps liquids from soaking through the cup. The process does not require a plastic film, which makes the cup easier to recycle. The chemical makeup of the dispersion is important. It contains emulsifiers and hydrophobic materials. These ingredients work together to block water, grease, and oil. You get a cup that holds both hot and cold drinks without leaking. The absence of a plastic film means you can recycle these cups in standard paper streams. This method supports the growing demand for water barrier coated cups and sustainable packaging. Tip: The dispersion technique not only improves recyclability but also helps you meet strict environmental standards. Key Benefits for Food Packaging Switching to a water based coating paper cup brings several advantages for food packaging. First, you avoid plastic entirely. The coating dissolves back into water during recycling, so it does not create microplastics. This feature allows you to recover up to 99% of the paper fibers, making the cup fully recyclable. You also meet the requirements of regulations like SUPD and PPWR, since the coating does not count as a plastic layer under EU rules. Here are some key benefits you gain when you choose a water based coating paper cup: Plastic-Free Solution: You eliminate the need for traditional plastic films, which helps your business align with new environmental laws. High Recyclability: The coating allows almost all paper fibers to be recovered, so you can recycle these cups with regular paper products. Improved Compostability: The coating breaks down more easily than plastic, which supports better waste management and composting. Enhanced Performance: The barrier resists water, grease, and oil, so your drinks and foods stay contained without leaks or soggy paper. You play a role in reducing plastic waste and supporting a circular economy when you use barrier coating for paper cups. This approach also helps you build a positive brand image. Customers notice when you choose eco-friendly options like paper cup coating. As more businesses and consumers look for sustainable choices, water based coating paper cup solutions stand out as a smart and responsible option.   Water-Based vs PE and PLA Coatings Composition and Application Differences You need to understand how the materials in paper cup coatings differ. Water-based coatings use a blend of water, natural materials like starch and cellulose, minerals, and some synthetic polymers. PE coatings rely on polyethylene, a type of plastic. PLA coatings come from renewable resources such as corn starch. Here is a table that shows the differences in composition and application: Coating Type Composition Details Environmental Impact Performance Characteristics Water-Based Blend of water, natural materials (starch, cellulose), minerals, synthetic polymers Biodegradable, eco-friendly Compostable, suitable for various applications PE Polyethylene Non-biodegradable, recycling challenges Excellent moisture and grease resistance PLA Derived from renewable resources (corn starch) Biodegradable under industrial composting Food grade, high strength, resistance to heat, water, and grease You see that water-based coatings offer a plastic-free solution. You can apply them directly to paperboard using a dispersion technique. PE and PLA coatings require extrusion or lamination, which adds complexity to manufacturing. Water-based coatings make recycling easier because they do not create microplastics. Another table highlights application differences: Coating Type Durability Environmental Impact Cost Compostability Ideal Use Case PE High Poor Low No Cost-driven mass production PLA Medium Good Medium Industrial composting Sustainable brands Water-Based Medium Excellent Medium-High Yes Eco-friendly packaging You can see that water-based coatings fit best for eco-friendly packaging and brands that value sustainability. PE coatings suit mass production where cost matters most. PLA coatings work for brands that want renewable materials but need industrial composting.     Efficiency and Performance You want your paper cup coating to perform well and stay cost-effective. PE coatings offer the lowest cost and excellent performance. PLA coatings cost more but provide good strength and resistance. Water-based coatings cost the most but match PE in performance. Here is a comparison table: Feature PE Coating PLA Coating Water-Based Coating Cost Lowest Medium Highest Performance Excellent Good Excellent You notice that water-based coatings deliver excellent performance. They resist water, grease, and oil, making them suitable for hot and cold drinks. PE coatings have high durability and moisture resistance. PLA coatings offer moderate durability and moisture resistance. Another table shows performance metrics: Coating Type Durability Moisture Resistance Environmental Impact PE High Excellent Moderate PLA Medium Moderate High Water-Based Medium Low Very High You see that water-based coatings excel in environmental impact. PE coatings last longer and resist moisture better, but they pose recycling challenges. PLA coatings perform well but need special composting facilities. Note: Water-based coatings help you meet strict environmental standards without sacrificing performance. You can use water barrier coated cups for a wide range of beverages and foods.   Environmental Impact You want to choose a coating that supports sustainability. Water-based coatings stand out because they work with modern recycling systems. You can recycle them with regular paper, which enhances their recyclability. PE coatings create recycling challenges, and PLA coatings need industrial composting. Water-based coatings can be repulped during recycling. You reduce waste and maintain cup strength. You find water-based coatings more compatible with recycling systems than PE and PLA coatings. Water-based coatings lower the environmental footprint. You enable better recycling and reduce energy use during production. PLA coatings require industrial composting. PE coatings are difficult to recycle and pose sustainability challenges. You play a key role in reducing waste when you choose barrier coating for paper cups. Water-based coatings support a circular economy and help your business meet environmental goals. Customers appreciate eco-friendly choices like water based coating paper cup solutions. You build trust and show responsibility by selecting sustainable packaging.   Food Safety and Microplastics Food Contact Safety Standards You want your water based coating paper cup to meet strict food safety standards. Manufacturers design these coatings to avoid harmful chemicals. You can see the main features in the table below: Feature Description Non-toxic Water-based coatings are free from harmful chemicals like PFAS, BPA, and VOCs. Biodegradable These coatings are eco-friendly and compostable, making them sustainable. Moisture and oil resistance They provide high resistance to moisture and oil, essential for food safety. You can trust water barrier coated cups to protect your drinks and foods. These coatings resist moisture and oil, so your food stays safe. You avoid exposure to toxic substances. You also support sustainability because the coatings break down naturally. Tip: Always check if your paper cup coating meets recognized food contact standards. This helps you ensure safety for your customers. Studies show that migration of chemicals depends on the type of food and the medium. You can see the findings in the table below: Study Findings Key Factors Influencing Migration Xu et al. (2010) Phthalate migration varied significantly, with higher rates in edible oils compared to mineral water. Lipophilic properties of food Baele et al. (2020) Higher migration levels in high-fat foods like chocolate and biscuits. Fat content of food Kubwabo et al. (2009) BPA migration rates differed between ethanol and water, indicating medium influence. Medium of contact (water vs. ethanol) You see that water-based coatings minimize migration risks, especially when compared to plastic linings.   Microplastics and Health Concerns You want to avoid microplastics in your barrier coating for paper cups. Water based coating paper cup solutions help you achieve this goal. Here are the main ways these coatings address microplastic concerns: The elimination of polyethylene (PE) plastic linings reduces the risk of microplastics being released into beverages. Water-based coatings use safe materials for food contact and do not leach harmful chemicals. These coatings are compostable and recyclable, contributing to sustainability and reducing plastic waste. Microplastics pose health risks. You should know the facts: Microplastics can release harmful chemicals like phthalates, PFAS, and BPA into food, which are known endocrine disruptors. These chemicals have been linked to various health issues, including cancer and reproductive problems. A 2023 study indicated that prenatal exposure to phthalates can lead to behavioral and learning disorders in children. Microplastics have been detected in various human body parts, raising concerns about their health impacts. You protect your customers when you choose water barrier coated cups. You reduce the risk of microplastics and harmful chemicals. You also support a healthier environment with sustainable paper cup coating options.   Recyclability and End-of-Life Recycling Water Based Coating Paper Cup You can recycle water based coating paper cup products easily. These cups fit into standard paper recycling streams. Facilities sort them alongside regular paper, and you do not need extra treatment. The recycling technology already exists, so you can repulp these cups without difficulty. Many recycling centers classify them under the PAP 22 code, which means you avoid complex separation steps. You help reduce landfill waste when you choose water barrier coated cups. Cup Type Recycling Capability Water-Based Coated Cups Can be recycled in standard paper streams PE-Coated Cups Cannot be recycled due to the plastic layer PLA-Coated Cups Faces recycling issues similar to PE   Compostability and Biodegradability You support composting and biodegradation when you select barrier coating for paper cups. Water-based coatings break down naturally. You can compost these cups at home or in industrial facilities. The coating dissolves in water and integrates with paper fibers, so it does not leave harmful residues. You improve waste management and help create nutrient-rich compost. PE-coated cups do not compost, and PLA-coated cups require special industrial composting. Tip: Always check local composting guidelines to ensure proper disposal of paper cup coating products.   End-of-Life Comparison You make a positive environmental impact when you choose water barrier coated cups. The end-of-life outcomes differ for each coating type. Water-based cups recycle or compost easily. PE-coated cups usually end up in landfills. PLA-coated cups need industrial composting and often face recycling challenges. Aspect Water-Based PE-Coated PLA-Coated Recyclability High in paper streams Low/specialized Limited Compostability Yes None Industrial only Common End Recycle/compost Landfill Landfill/compost Water-based barrier coated cups are fully water-soluble and integrate with fiber. You can dispose of them in standard mixed-paper or cardboard recycling bins. You help close the loop in packaging sustainability when you use water based coating paper cup solutions. You support recycling, composting, and a cleaner environment.   Real-World Performance Barrier Properties and Liquid Holdout You expect water barrier coated cups to keep drinks contained without leaks. Water-based barrier coatings form a strong layer on the paperboard. This layer prevents water from soaking through, even with hot or cold beverages. You can rely on these cups for coffee, tea, or juice. The coating maintains the cup’s shape and strength, so you avoid soggy paper and spills. Manufacturers design water based coating paper cup products to match the performance of traditional plastic linings. You get reliable liquid holdout and a sustainable solution. Tip: Water-based coatings help you serve drinks confidently, knowing the cup will not fail during use.   Grease and Oil Resistance You need barrier coating for paper cups that can handle greasy foods and oily drinks. Water-based barrier coatings create a plastic-free shield that resists grease, oil, and water. You find that these coatings perform as well as polyethylene, keeping liquids and oils inside the cup. The barrier composition gives substantial resistance to oil and grease, so you avoid leaks and stains. Description Type of Resistance The coating resists water, oil, and grease. Substantial resistance Water, oil, and grease cannot easily go through the barrier coating. Effective barrier The barrier composition gives resistance to oil, grease, and water. Effective barrier You can use water based coating paper cup solutions for beverages with fatty acids. The cups maintain their structure and prevent leaks, even with oily substances. Compared to polyethylene coatings, water-based options are easier to recycle and more eco-friendly.   User Experience You notice several benefits when you choose water barrier coated cups. The water-based dispersion coating protects paper from moisture and supports composting or recycling. You do not need to separate layers, which simplifies disposal. These cups meet strict safety standards and receive FDA approval for food contact. Businesses appreciate the appeal of compostable and recyclable materials. Innovations in renewable resources and water-based barrier systems enhance sustainability. Water-based coating is eco-conscious and protects paper from moisture. Cups can be composted or recycled without separating layers. Approved for food contact by the FDA. Higher production costs due to complex application. May not suit all products, such as carbonated beverages. You help your business stand out by using paper cup coating that supports environmental goals. Customers value the sustainable choice and enjoy a reliable, safe drinking experience.   Regulatory Compliance Global Regulations Overview You need to understand the global regulations that affect water based coating paper cup solutions. These rules help you ensure safety and sustainability for your products. Many countries set strict standards for food contact materials. You see agencies like the FDA in the United States and EFSA in Europe leading the way. Brazil uses ANVISA, while South America follows Mercosur guidelines. National regulations in Germany, Switzerland, and Canada also play a role. Regulation Description FDA United States Food and Drug Administration regulations for food safety. EFSA European Food Safety Authority regulations applicable in the EU. ANVISA Brazilian Health Regulatory Agency standards. Mercosur Regulations from the South American Common Market. National regulations Various national regulations from countries like Germany, Switzerland, and Canada. You must check these regulations before choosing a barrier coating for paper cups. Each region sets its own requirements for paper cup coating and water barrier coated cups. You protect your customers and your business by following these rules.   Certifications and Standards You want your water based coating paper cup to meet recognized certifications and standards. These certifications show that your products are safe for food contact and meet environmental goals. You should look for compliance with FDA 176.170 for direct food contact in North America. In Europe, Bfrxxxvi is the standard for direct food contact. Your cups must also show heat resistance up to 176°F. FDA 176.170 compliance for North America Bfrxxxvi compliance for Europe Heat resistance up to 176°F You can ask suppliers for certificates and test reports. These documents prove that your water barrier coated cups meet all safety and quality standards. You build trust with customers when you use certified barrier coating for paper cups. You also avoid legal risks and support sustainable packaging. Tip: Always verify certifications before sourcing paper cup coating solutions. This step helps you ensure compliance and quality.   Choosing the Right Solution Assessing Business Needs You need to evaluate your business requirements before selecting a water based coating paper cup solution. Start by considering key criteria that affect both performance and sustainability. The table below helps you compare important factors: Criteria Description Packaging approval requirements Focus on material composition and recyclability early in design. Recycling and fiber recovery focus Choose coatings that support fiber recovery and fit recycling systems. Water-based coating adoption Look for solutions that apply easily on existing production lines. Multifunctional coating solutions Seek coatings that protect against grease, moisture, and allow heat sealing in one layer. Sustainable foodservice packaging Select coatings that boost performance and support recycling goals. Low-coating-weight technologies Prefer coatings that deliver barriers with less material and lower drying needs. Lengthy approval process Ensure coatings perform well during production and storage to avoid delays. Food-contact compliance requirements Confirm coatings meet food safety and regulatory standards for your market. Production efficiency challenges Check for suitable drying capacity and stable conditions for water-based coatings. You should also weigh procurement considerations. Water-based coatings are eco-friendly and break down easily in nature, reducing waste. However, they often cost more than traditional PE coatings. Some coatings may not match PE in heat or grease resistance, which can limit use for certain foods or drinks. Availability may be limited, so sourcing can take extra time. Always consider regulatory readiness, product safety, heat performance, and how consumers view your packaging.   Sourcing and Supplier Tips When you source water barrier coated cups or barrier coating for paper cups, ask suppliers detailed questions to ensure you get the right product. Use the table below to guide your discussions: Supplier Claim Follow-Up Question “Hot cup grade” What beverage temperature, hold time, and cup format was this designed for? “Food grade” Which product, coating, use condition, and target market does the documentation cover? “Compostable” What certification or test evidence supports this, and does it apply to the full cup and coating? “Recyclable” In which market or collection system is this claim intended to apply? “Leakproof” What testing method or service condition supports the claim? “Suitable for coffee” Does that include milk-based, sweetened, or extended-hold beverages? “Eco” or “sustainable” Which specific attribute is being claimed, and what evidence supports that wording?   You should request certifications and test reports for any paper cup coating. Brands like elementscup provide documentation for food safety, compostability, and recyclability. This helps you verify claims and ensures your water based coating paper cup meets all standards. By asking the right questions, you can confidently choose water barrier coated cups that align with your business goals and sustainability values. You gain several advantages when you choose water based coating paper cup solutions: Water barrier coated cups offer a plastic-free, recyclable option that meets food safety standards. You help reduce landfill waste by allowing cups to be sorted with regular paper. Barrier coating for paper cups supports your brand’s environmental goals and aligns with consumer demand for eco-friendly products. Solenis and other providers offer paper cup coating technologies that match traditional performance while improving sustainability. You can invest in equipment, secure renewable materials, and educate customers to support your transition. By adopting these solutions, you lead your business toward a greener future.   FAQ What makes a water based coating paper cup different from a regular paper cup? You get a water based coating paper cup that uses a plastic-free barrier. This coating keeps liquids inside the cup. Regular paper cups often use plastic linings, which make recycling harder. Can you recycle water barrier coated cups with regular paper? Yes, you can recycle water barrier coated cups in standard paper streams. The coating dissolves during recycling, so you recover most of the paper fibers. Always check your local recycling guidelines. Are barrier coating for paper cups safe for hot drinks? You can safely use barrier coating for paper cups with hot beverages. These coatings resist heat and prevent leaks. Manufacturers design them to meet strict food safety standards. Do paper cup coating solutions contain harmful chemicals? No, paper cup coating solutions avoid harmful chemicals like PFAS and BPA. You get a safe product for food contact. Always ask your supplier for safety certifications. How do water based coating paper cups help the environment? You help the environment by choosing water based coating paper cups. These cups reduce plastic waste, support recycling, and break down more easily than plastic-lined cups. Customers notice your commitment to sustainability.
  • The Shift to Sustainable Dining: Why Modern Food Packaging is Moving to Paper The Shift to Sustainable Dining: Why Modern Food Packaging is Moving to Paper Jul 26, 2026
    In today's food service industry, delivery and takeaway are no longer just optional conveniences—they are core components of business success. However, as takeout order volumes rise, so does consumer awareness of packaging waste. Traditional single-use plastics and polystyrene (Styrofoam) containers are rapidly being phased out worldwide due to environmental concerns and tightening government regulations. For restaurants, cafes, and catering businesses, switching to sustainable paper packaging is no longer just a trend—it is a vital business strategy.   1. The Environmental Imperative: Beyond Single-Use Plastics Traditional plastic containers can take centuries to break down, micro-fragmenting into ecosystems and oceans. In contrast, paper-based food packaging originates from renewable resources, such as FSC-certified forest wood pulp and fast-growing bamboo fibers. When paired with modern, eco-friendly barriers—such as aqueous (water-based) barrier coatings or PLA (Polylactic Acid) plant-based linings - paper containers provide: Industrial & Home Compostability: Breaking down naturally without leaving toxic residues. Reduced Carbon Footprint: Lower greenhouse gas emissions throughout the manufacturing lifecycle compared to petroleum plastics. PFAS-Free Safety: Elimination of harmful fluorinated "forever chemicals" while maintaining oil and water resistance.   2. High Performance Meets Practicality A common misconception in the past was that paper containers couldn't hold up against greasy or hot liquids. Today's manufacturing innovations have changed the game completely: Leak-Proof Soup & Beverage Cups: Double-wall and ripple-wall paper cups provide superior thermal insulation for hot drinks without needing extra sleeves, while engineered paper lids ensure a tight, spill-free seal. Grease & Water Resistance: Natural kraft paper food boxes and split-compartment bento containers are coated with food-grade aqueous barriers, keeping gravies and oils contained without sogginess. Microwave & Oven Safety: Unlike plastic containers that can warp or leach chemicals under high heat, high-spec paper food bowls can safely handle reheating.   3. Elevating Brand Identity Through Customization Packaging is often the very first physical touchpoint a customer has with your takeaway food. Plain, unbranded plastic containers communicate commodity; custom-printed, natural-textured paper packaging communicates quality, care, and sustainability. Customizing paper packaging allows food service brands to:   Showcase Eco-Commitment: Highlight your use of biodegradable materials directly on the container. Enhance Presentation: Clear window lunch boxes and clean, modern contours highlight the colors and freshness of your dishes. Build Brand Recognition: Vibrant, food-safe custom logos and custom color schemes make your food memorable and shareable on social media.   4. Choosing the Right Paper Packaging for Your Menu Different dishes require tailored packaging solutions to maintain heat, texture, and visual appeal: Food Category Recommended Paper Solution Key Benefit Hot Beverages & Soups Double-Wall Paper Cups & Paper Soup Containers Heat insulation, leak resistance, PFAS-free Salads & Fresh Meal Kits Kraft Window Lunch Boxes & Clear PET Lids High visual appeal, fresh preservation Burgers, Fries & Fried Foods Folding Kraft Cartons / Vented Cardboard Boxes Crispy texture protection, greaseproof lining Asian Cuisine & Bento Meals Multi-Compartment Paper Bento Boxes Prevents cross-flavor   Partner with Elements Packaging for Your Eco-Friendly Journey At Elements Packaging, we manufacture a complete suite of eco-friendly disposable packaging solutions—including FSC-certified paper cups, aqueous barrier coffee cups, kraft food boxes, paper soup bowls, and compostable cutlery. Engineered for durability and designed for the planet, our custom OEM/ODM packaging helps food service businesses worldwide transition seamlessly toward sustainability. Ready to upgrade your takeaway packaging? Contact our design team today to request custom samples and learn more about our wholesale solutions.
  • Small Choices, Big Impact: How Eco-Friendly Takeaway Packaging Drives Consumer Loyalty Small Choices, Big Impact: How Eco-Friendly Takeaway Packaging Drives Consumer Loyalty Jul 18, 2026
    In today's food economy, the dining experience doesn't end when a meal is packed away for delivery. Modern consumers are highly eco-conscious. When a takeaway order arrives encased in layers of non-recyclable polystyrene foam or heavy single-use plastics, it leaves a lingering sense of environmental guilt. As a premier paper food packaging manufacturer, Elements Packaging has watched this behavioral shift closely. Today, choosing sustainable packaging is no longer just a regulatory box to check—it is one of the most effective tools for building lasting customer loyalty. The Psychology of Sustainable Packaging When a customer unboxes a meal from a beautifully crafted, biodegradable paper lunch box or a natural Kraft paper noodle bowl, their perception of the restaurant instantly elevates. The organic texture and clean aesthetic of high-quality paper food packaging communicate a brand values story: We care about the ingredients we put into our food, and we care about the planet we leave behind. Many consumers are actively seeking out establishments that align with their green environmental practices. In fact, offering compostable or easily recyclable paper boxes and paper bags gives businesses a competitive edge that keeps customers clicking "order again." Seamless Functionality Meets Circular Economy A common worry for fast-casual businesses is whether eco-friendly alternatives can handle the rigorous demands of delivery drivers and delivery apps. Our specialized lines of microwaveable paper containers and oil-proof food paper trays prove that sustainability can be incredibly tough. They are explicitly designed to withstand high stacking loads, maintain temperature, and resist leaks. By switching to renewable pulp materials that naturally degrade or seamlessly re-enter the recycling loop, your food business actively reduces greenhouse gas emissions and diverts waste from landfills. Together, let us push the boundaries of the food industry toward a greener, more sustainable future.
1 2 3 4 5

A total of5pages

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Submit

Home

Products

whatsApp

contact